TipTrak Comes to North America
The first TipTrak in North America is manufactured by FGMCL, UniTrak’s predecessor. This marks the beginning of the technology’s North American history, two years before UniTrak Corporation Limited is founded.
UniTrak is a family-owned manufacturer of specialty conveying equipment for difficult bulk materials. More than five decades of application engineering, manufacturing and service experience help us protect your product, solve handling problems and support equipment throughout its working life.
Difficult Materials. Proven Solutions.
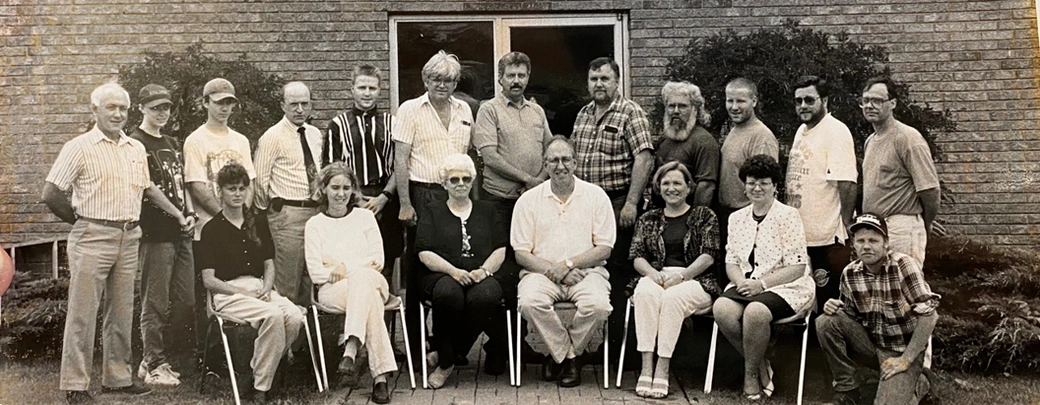
Since 1969, UniTrak has designed, manufactured and supported conveying equipment for difficult bulk materials. Experience across industries and generations of equipment helps our team connect material behaviour with practical conveying solutions.
Explore the milestones behind that experience.
The first TipTrak in North America is manufactured by FGMCL, UniTrak’s predecessor. This marks the beginning of the technology’s North American history, two years before UniTrak Corporation Limited is founded.
UniTrak Corporation Limited is founded on September 1, 1969. A North American representative network is established alongside the company, connecting customers with the business and its conveying technology.
UniTrak supplies a TipTrak to Johns Manville. This early installation forms part of the company’s history of applying bucket conveying technology to industrial material-handling requirements.
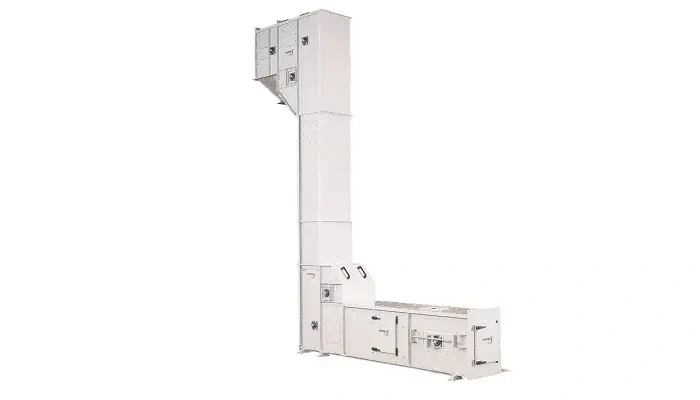
The first Monocoque TipTrak is sold. This enclosed construction expands the TipTrak range, providing another equipment configuration for applications requiring containment around the conveying path.
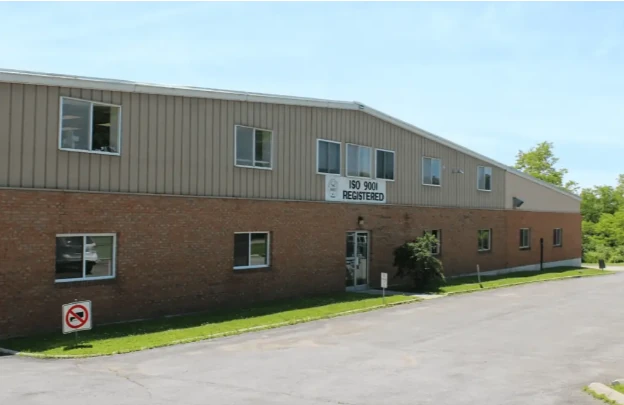
UniTrak builds a new factory and office and introduces the UniFlex conveyor. The milestone expands both the company’s manufacturing facilities and its technology range, adding screw conveying alongside TipTrak bucket conveying.
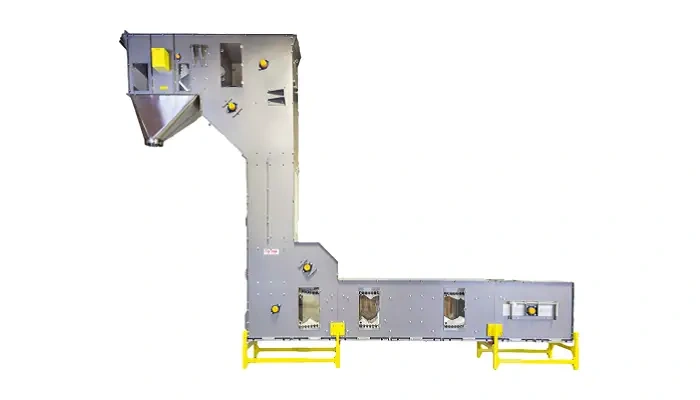
The Partially Enclosed Construction, or PEC, TipTrak is introduced. It adds another construction option to the range, giving customers a different approach to enclosing the bucket assembly.
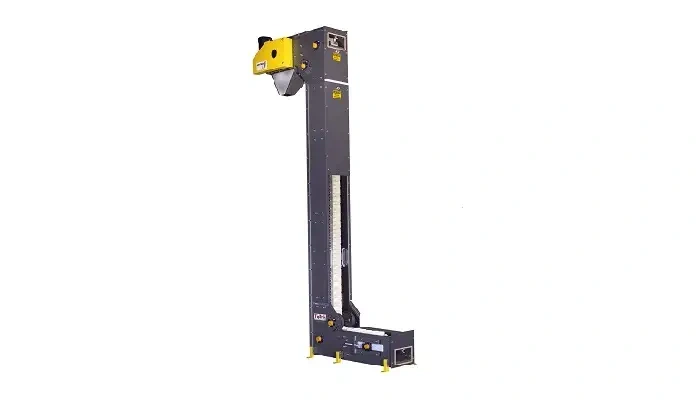
The TipTrak 500 bucket size is introduced. This addition broadens the TipTrak range and gives UniTrak another size to match conveying equipment to the material and required throughput.
UniTrak’s North American facility achieves ISO 9001 certification. The milestone marks an important development in the company’s quality management practices as it continues designing and manufacturing conveying equipment.
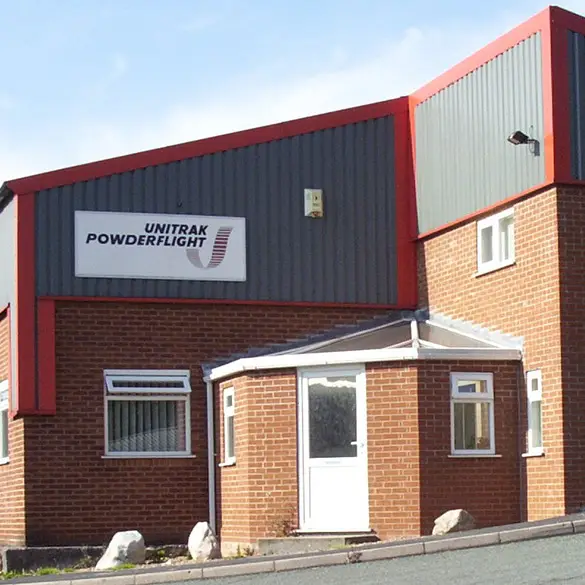
UniTrak establishes its European operation through the acquisition and incorporation of its United Kingdom subsidiary. The expansion adds a UK base to the company’s operations and strengthens its international presence.
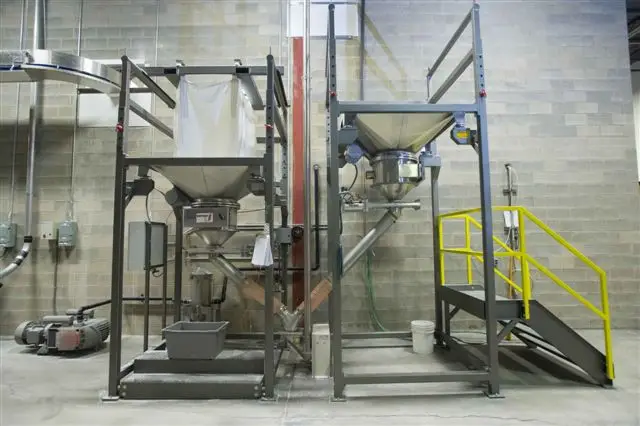
The Bagstander product line is introduced, expanding UniTrak’s capabilities into bulk bag handling. It adds equipment for another stage of the material-handling process alongside the company’s conveying technologies.
A UniTrak licensee is appointed in Australia. This milestone extends the company’s international reach and adds an Australian relationship to its growing network.
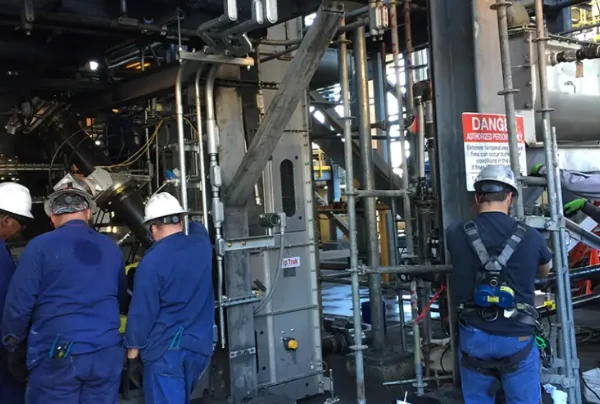
UniTrak formally adopts lean manufacturing practices. The initiative brings a structured focus on efficient production and continuous improvement into the company’s manufacturing operations.
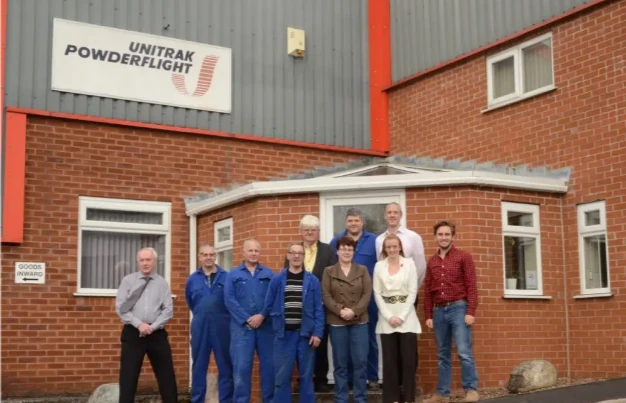
UniTrak’s United Kingdom facility achieves ISO 9001 certification. This adds a quality management milestone for the UK operation, following the North American facility’s certification in 1996.
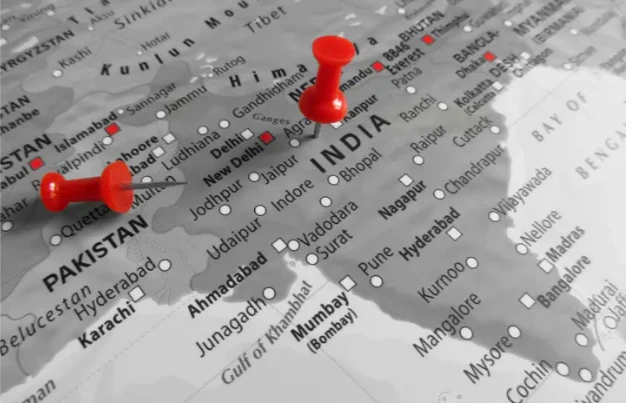
A UniTrak licensee is appointed in India. The appointment extends the company’s international presence into another market, following earlier expansion into Europe and Australia.
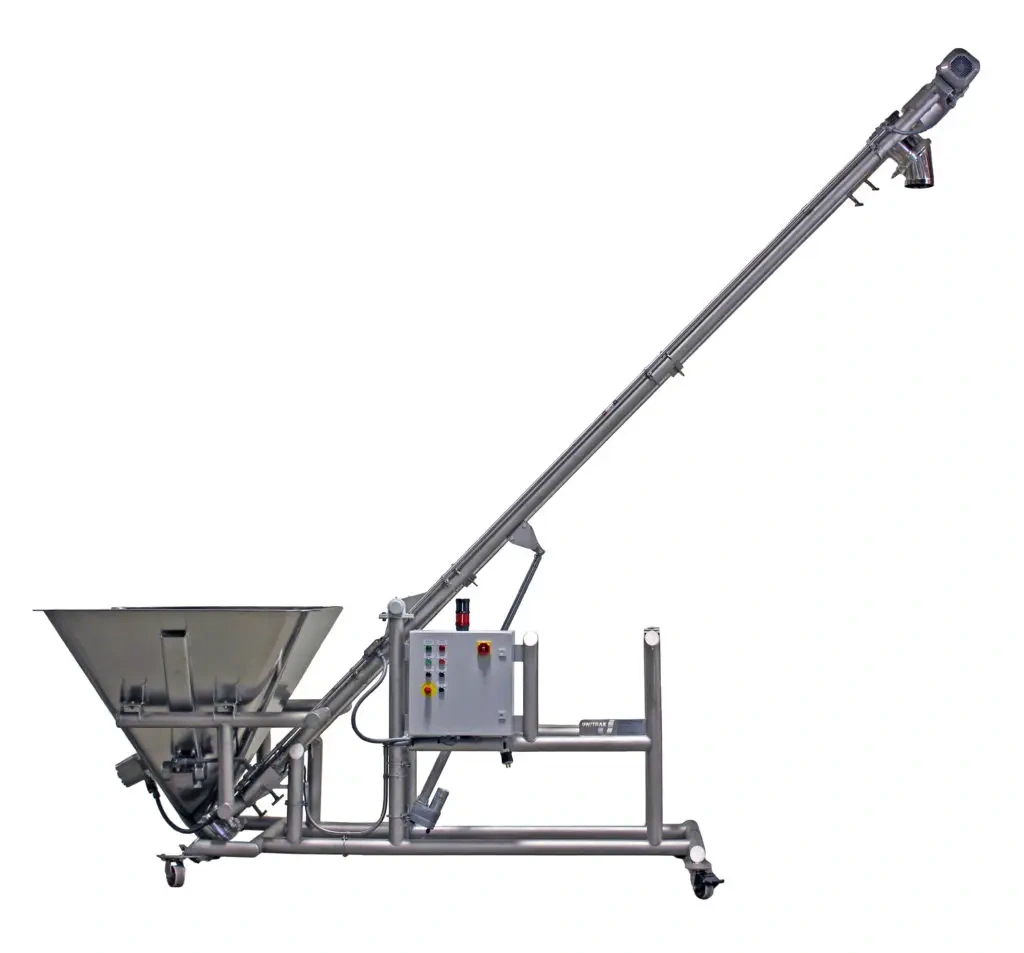
The UniFlex Easy-Clean model is introduced. It adds an option focused on cleaning access to the UniFlex range, expanding the configurations available for applications where cleanability matters.
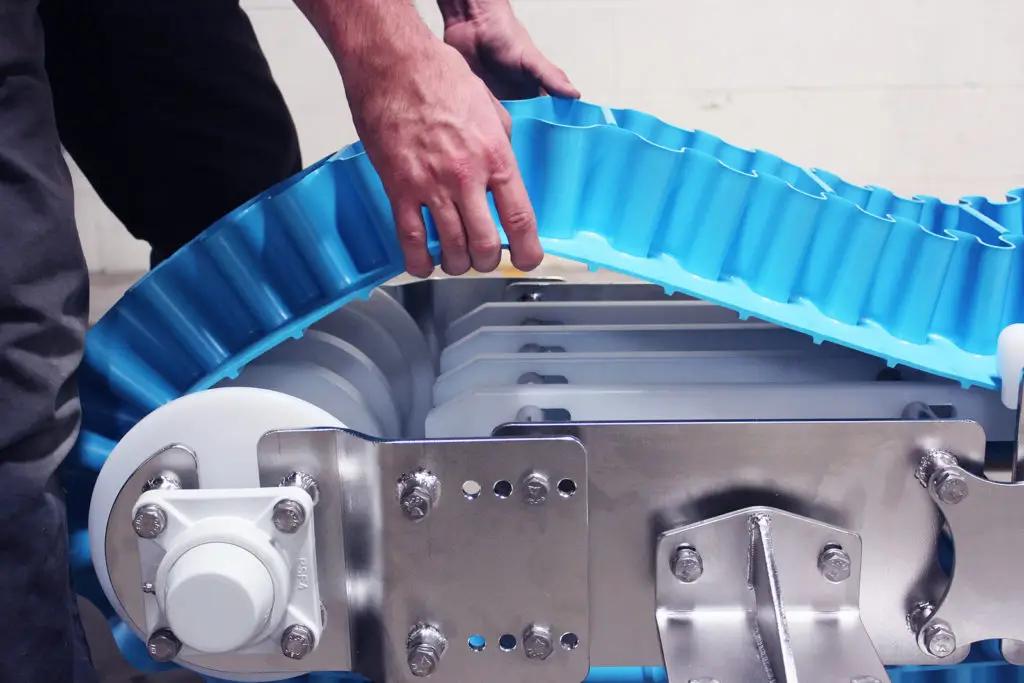
KleanTrak is introduced, adding a sanitary belt conveyor to UniTrak’s equipment range. Its focus on cleaning access and hygienic applications broadens the conveying approaches available to customers.
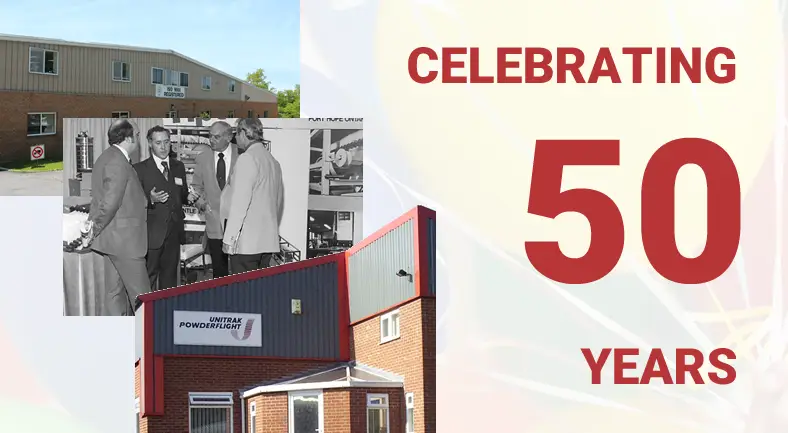
UniTrak celebrates its 50th anniversary. The milestone brings together five decades of application engineering, manufacturing and customer support, with a product range that has expanded beyond its original TipTrak technology.
Bill Gorsline retired, and Emma Gorsline took over leadership of UniTrak, becoming the second generation of the Gorsline family to lead the business.
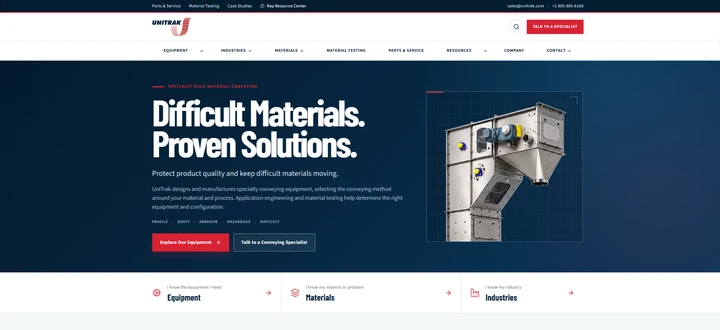
UniTrak launched a new website showcasing its conveying equipment, material-handling applications and technical resources.
UniTrak remains a family-owned business, with President Emma Gorsline representing the second generation of Gorsline family ownership following her father, Bill.
That continuity supports a long-term approach to customer relationships and the equipment we build. Application engineering, manufacturing and Parts & Service work together to help customers select conveying equipment and support it throughout its working life.
A successful conveying system begins before equipment is designed.
UniTrak works to understand the material, the process and what the customer is trying to accomplish.
Review its physical characteristics and the handling problem.
Establish the starting point, destination and surrounding equipment.
Confirm throughput, route, product condition, cleaning and containment needs.
Use actual-material testing where it will help resolve equipment-selection questions.
A conveying trial shows how your material feeds, moves and discharges in the equipment being evaluated. The findings help guide equipment selection and configuration.
Contact UniTrak before sending samples; an SDS and safety review are required.
LEARN ABOUT MATERIAL TESTINGDevelop the equipment configuration, connections and controls around the agreed scope.
Manufacturing, commissioning and service experience inform how we develop and support equipment. Our teams use that knowledge to improve future applications and help customers keep installed systems operating.
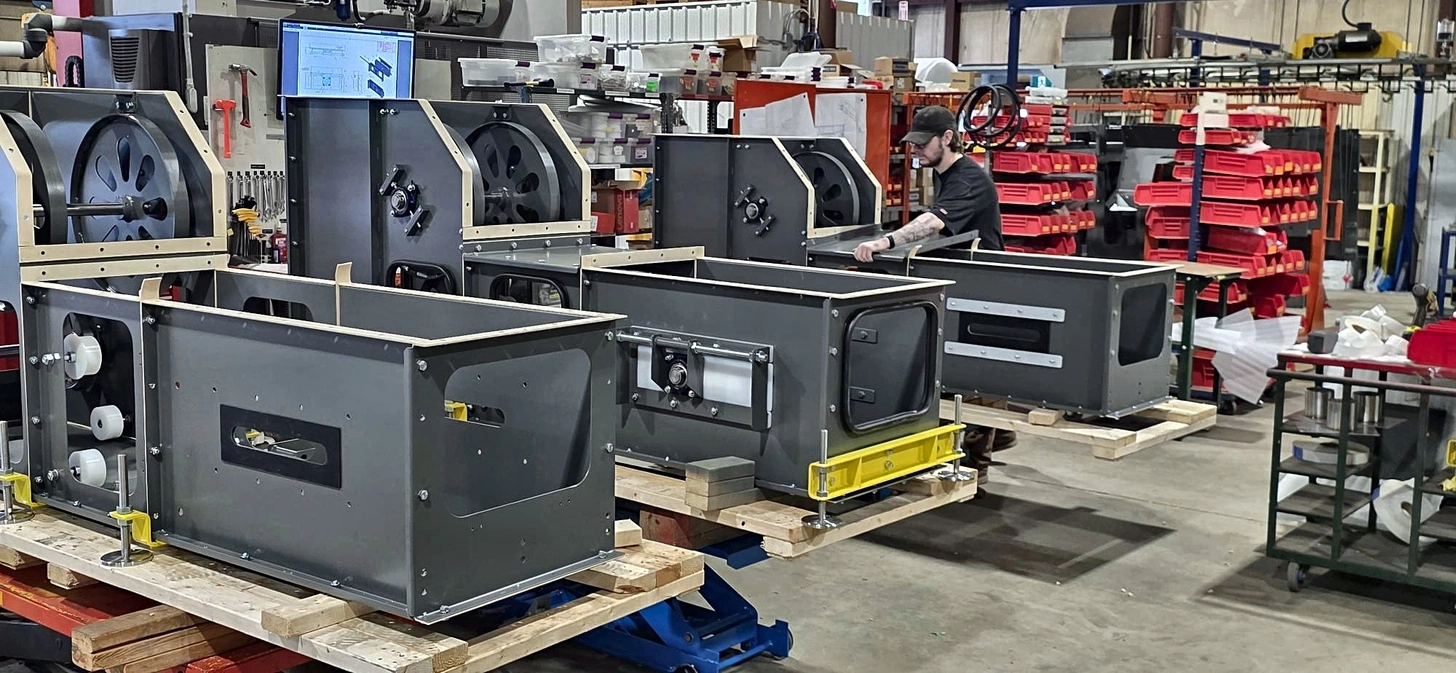
The people building the equipment have direct knowledge of the design and application requirements.
Proper startup, operation and maintenance help equipment perform as intended over the long term.
Customers have access to technical support, field service, preventative maintenance and replacement parts throughout the working life of their equipment.
Experience from manufacturing, testing, commissioning and equipment operating in the field contributes to the knowledge UniTrak applies to future applications.
UniTrak is an active member of PEMA, PMMI and SHAPA, connecting our team with the process equipment, packaging and solids handling industries.
Good equipment matters. So does the organization standing behind it.