Case Study
TipTrak™ Bucket Elevator Prevents Breakage in Packaging Application
See how a TipTrak™ bucket elevator protected fragile biodegradable packaging valves through gentle handling and zero breakage conveying performance.
In this case study
The Challenge
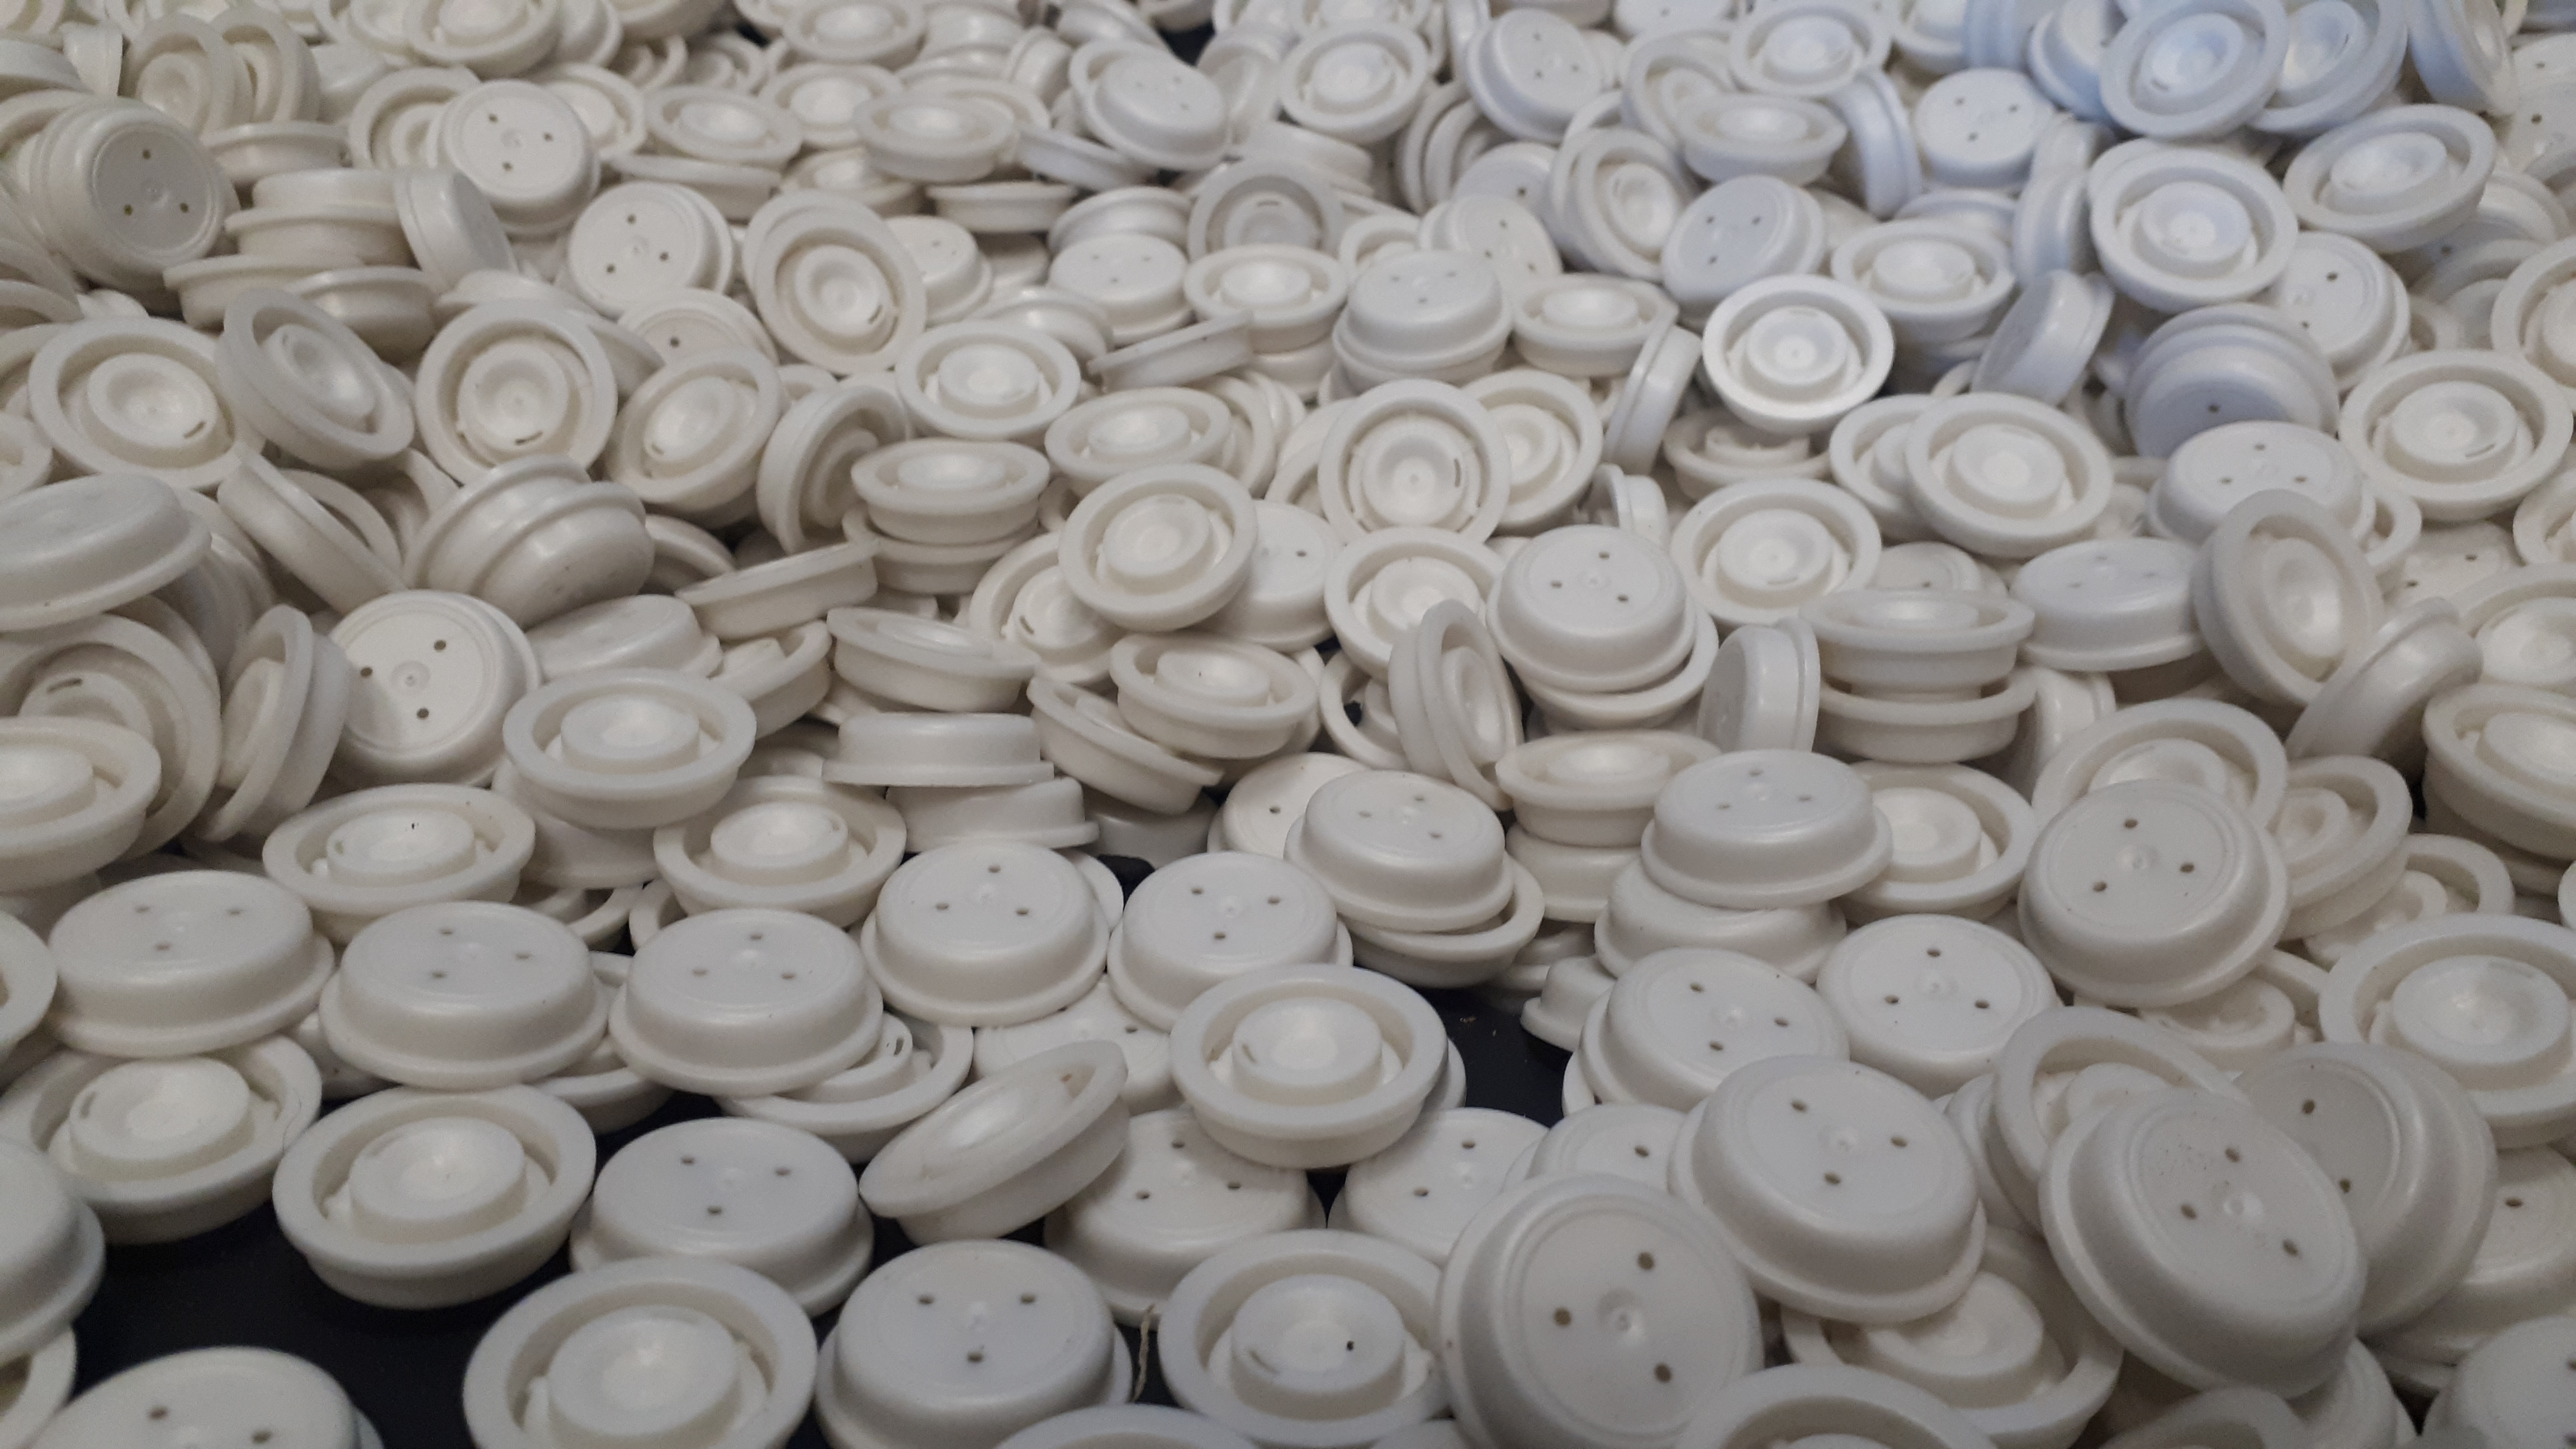
The project required conveying biodegradable packaging valves from a manual box dump station to downstream packaging equipment.
Several requirements had to be addressed:
• Maintain product integrity throughout transfer
• Support variable feed rates for downstream packaging equipment
• Provide portability for production flexibility
• Reduce line interruptions caused by damaged material
Traditional conveying systems risked product degradation and contamination within the packaging process. The customer needed a gentle handling solution capable of moving fragile components without damage.
The Solution and Results
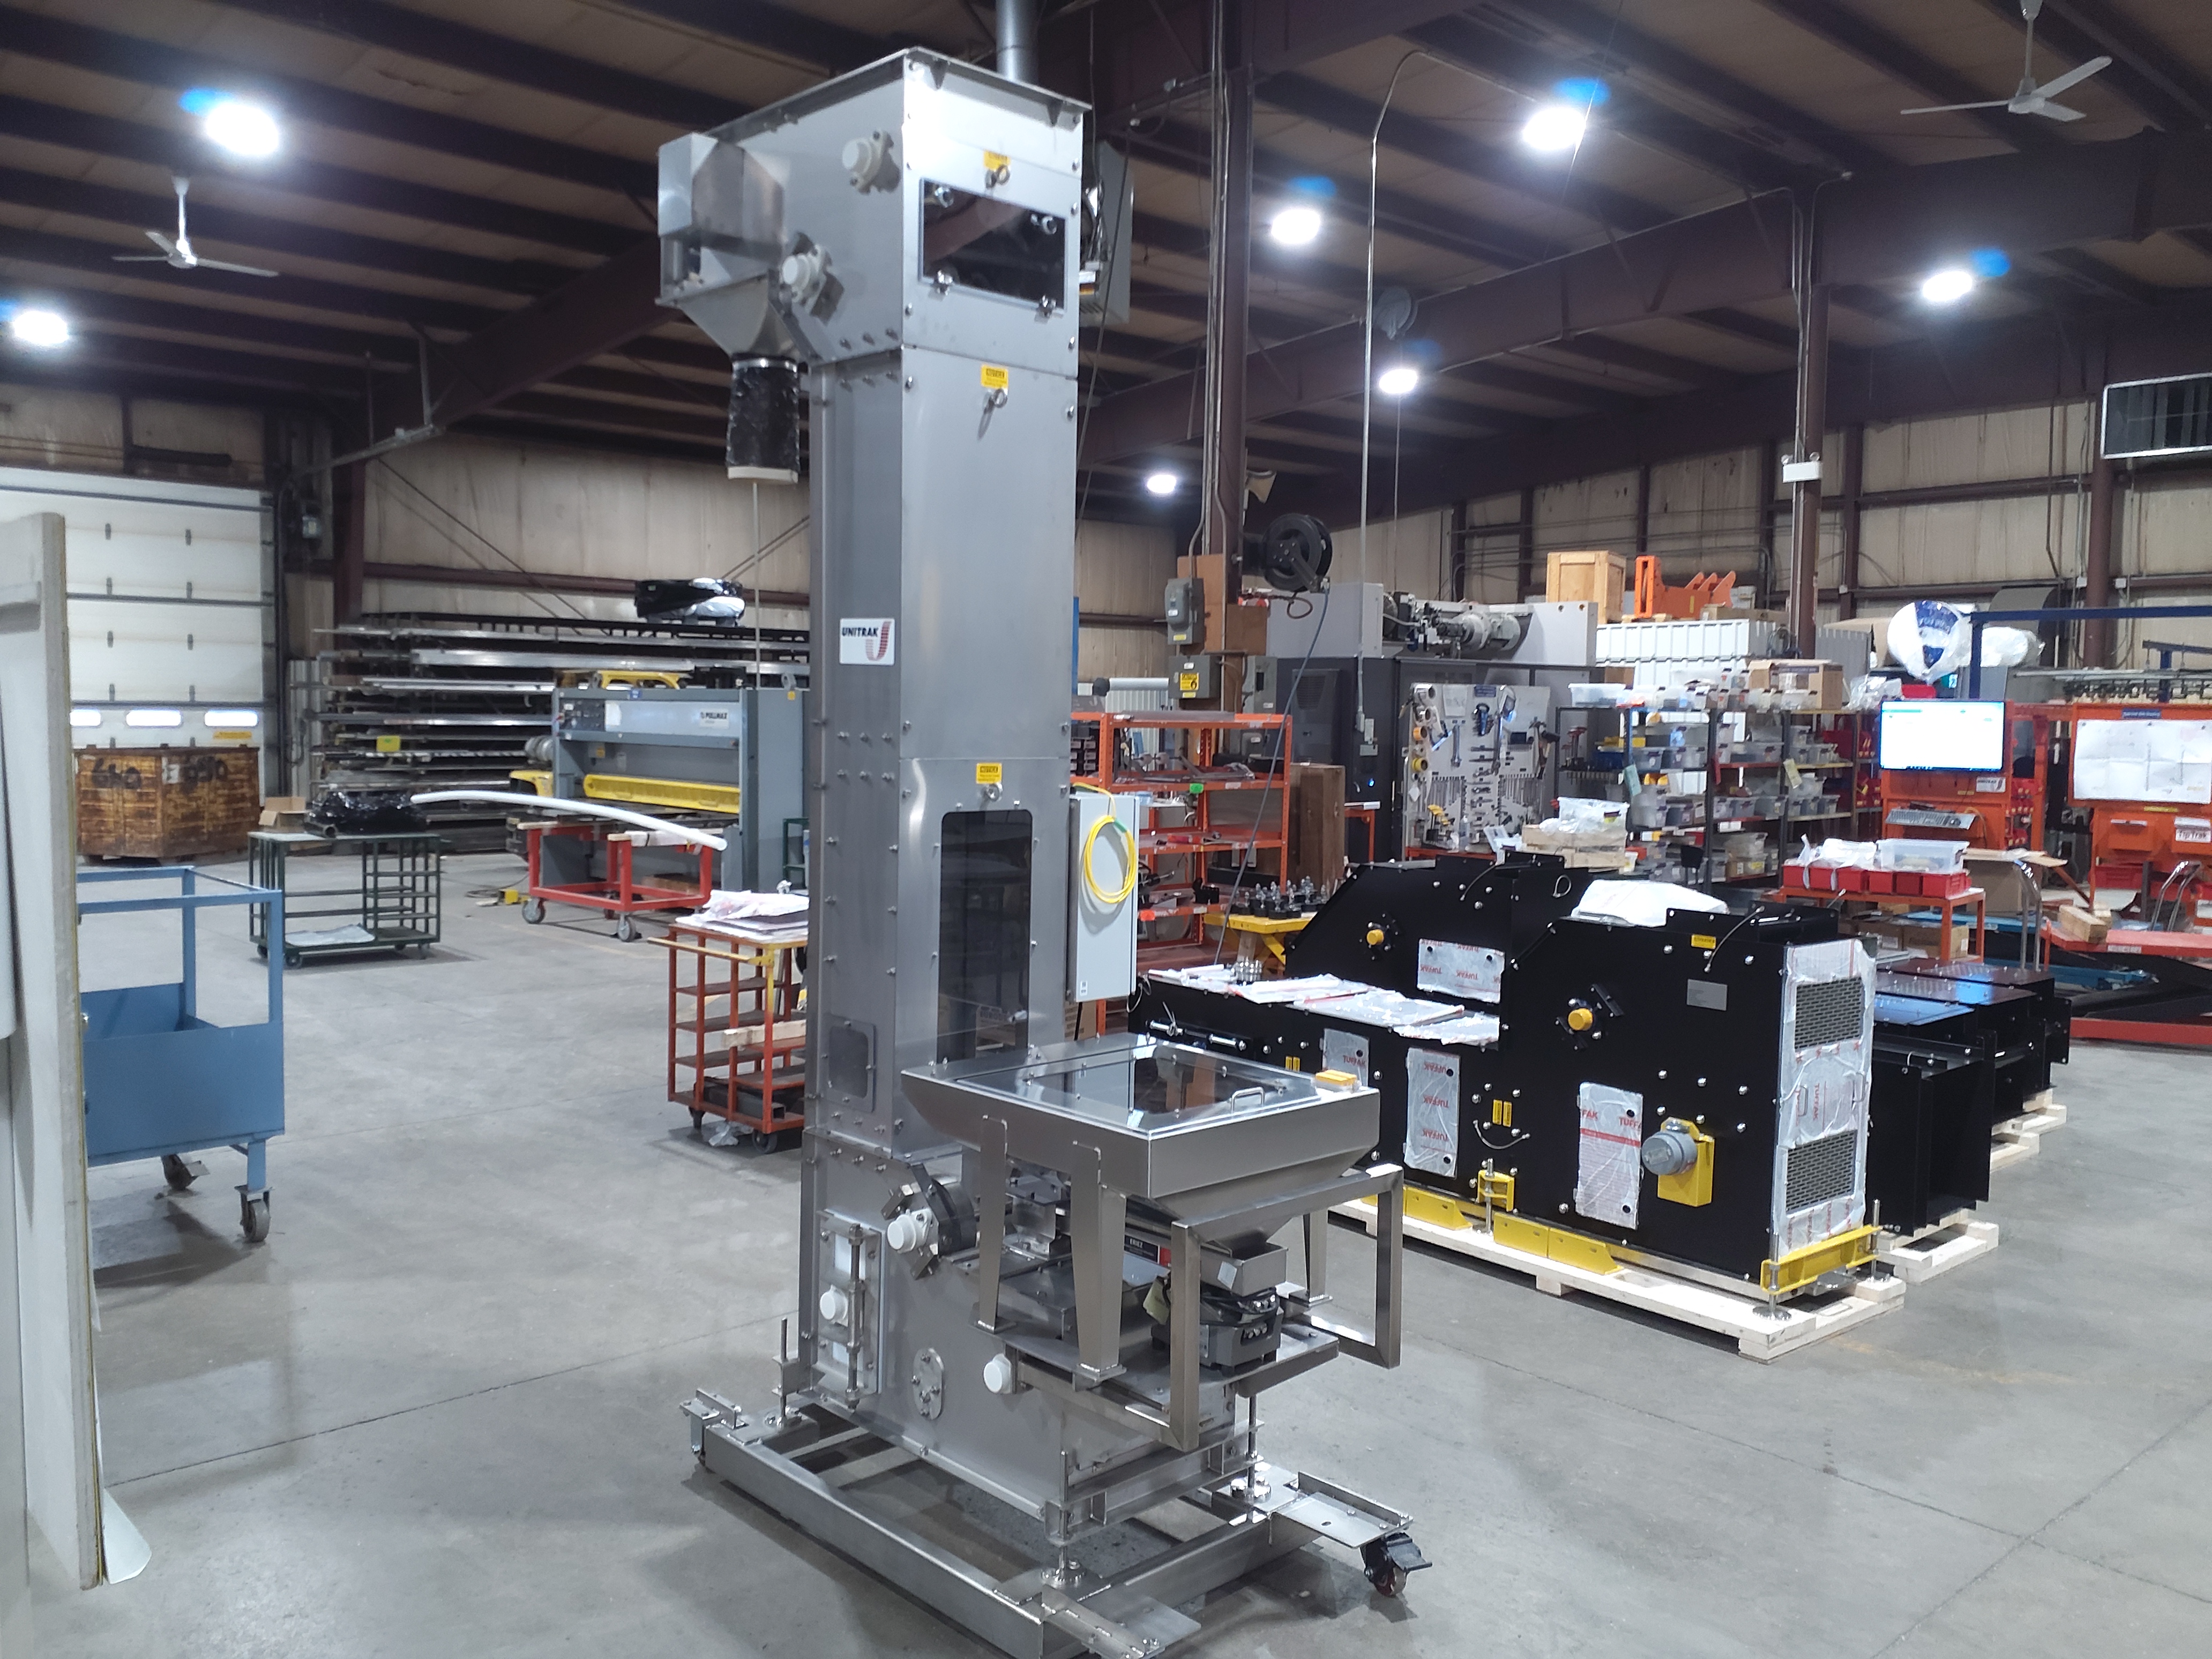
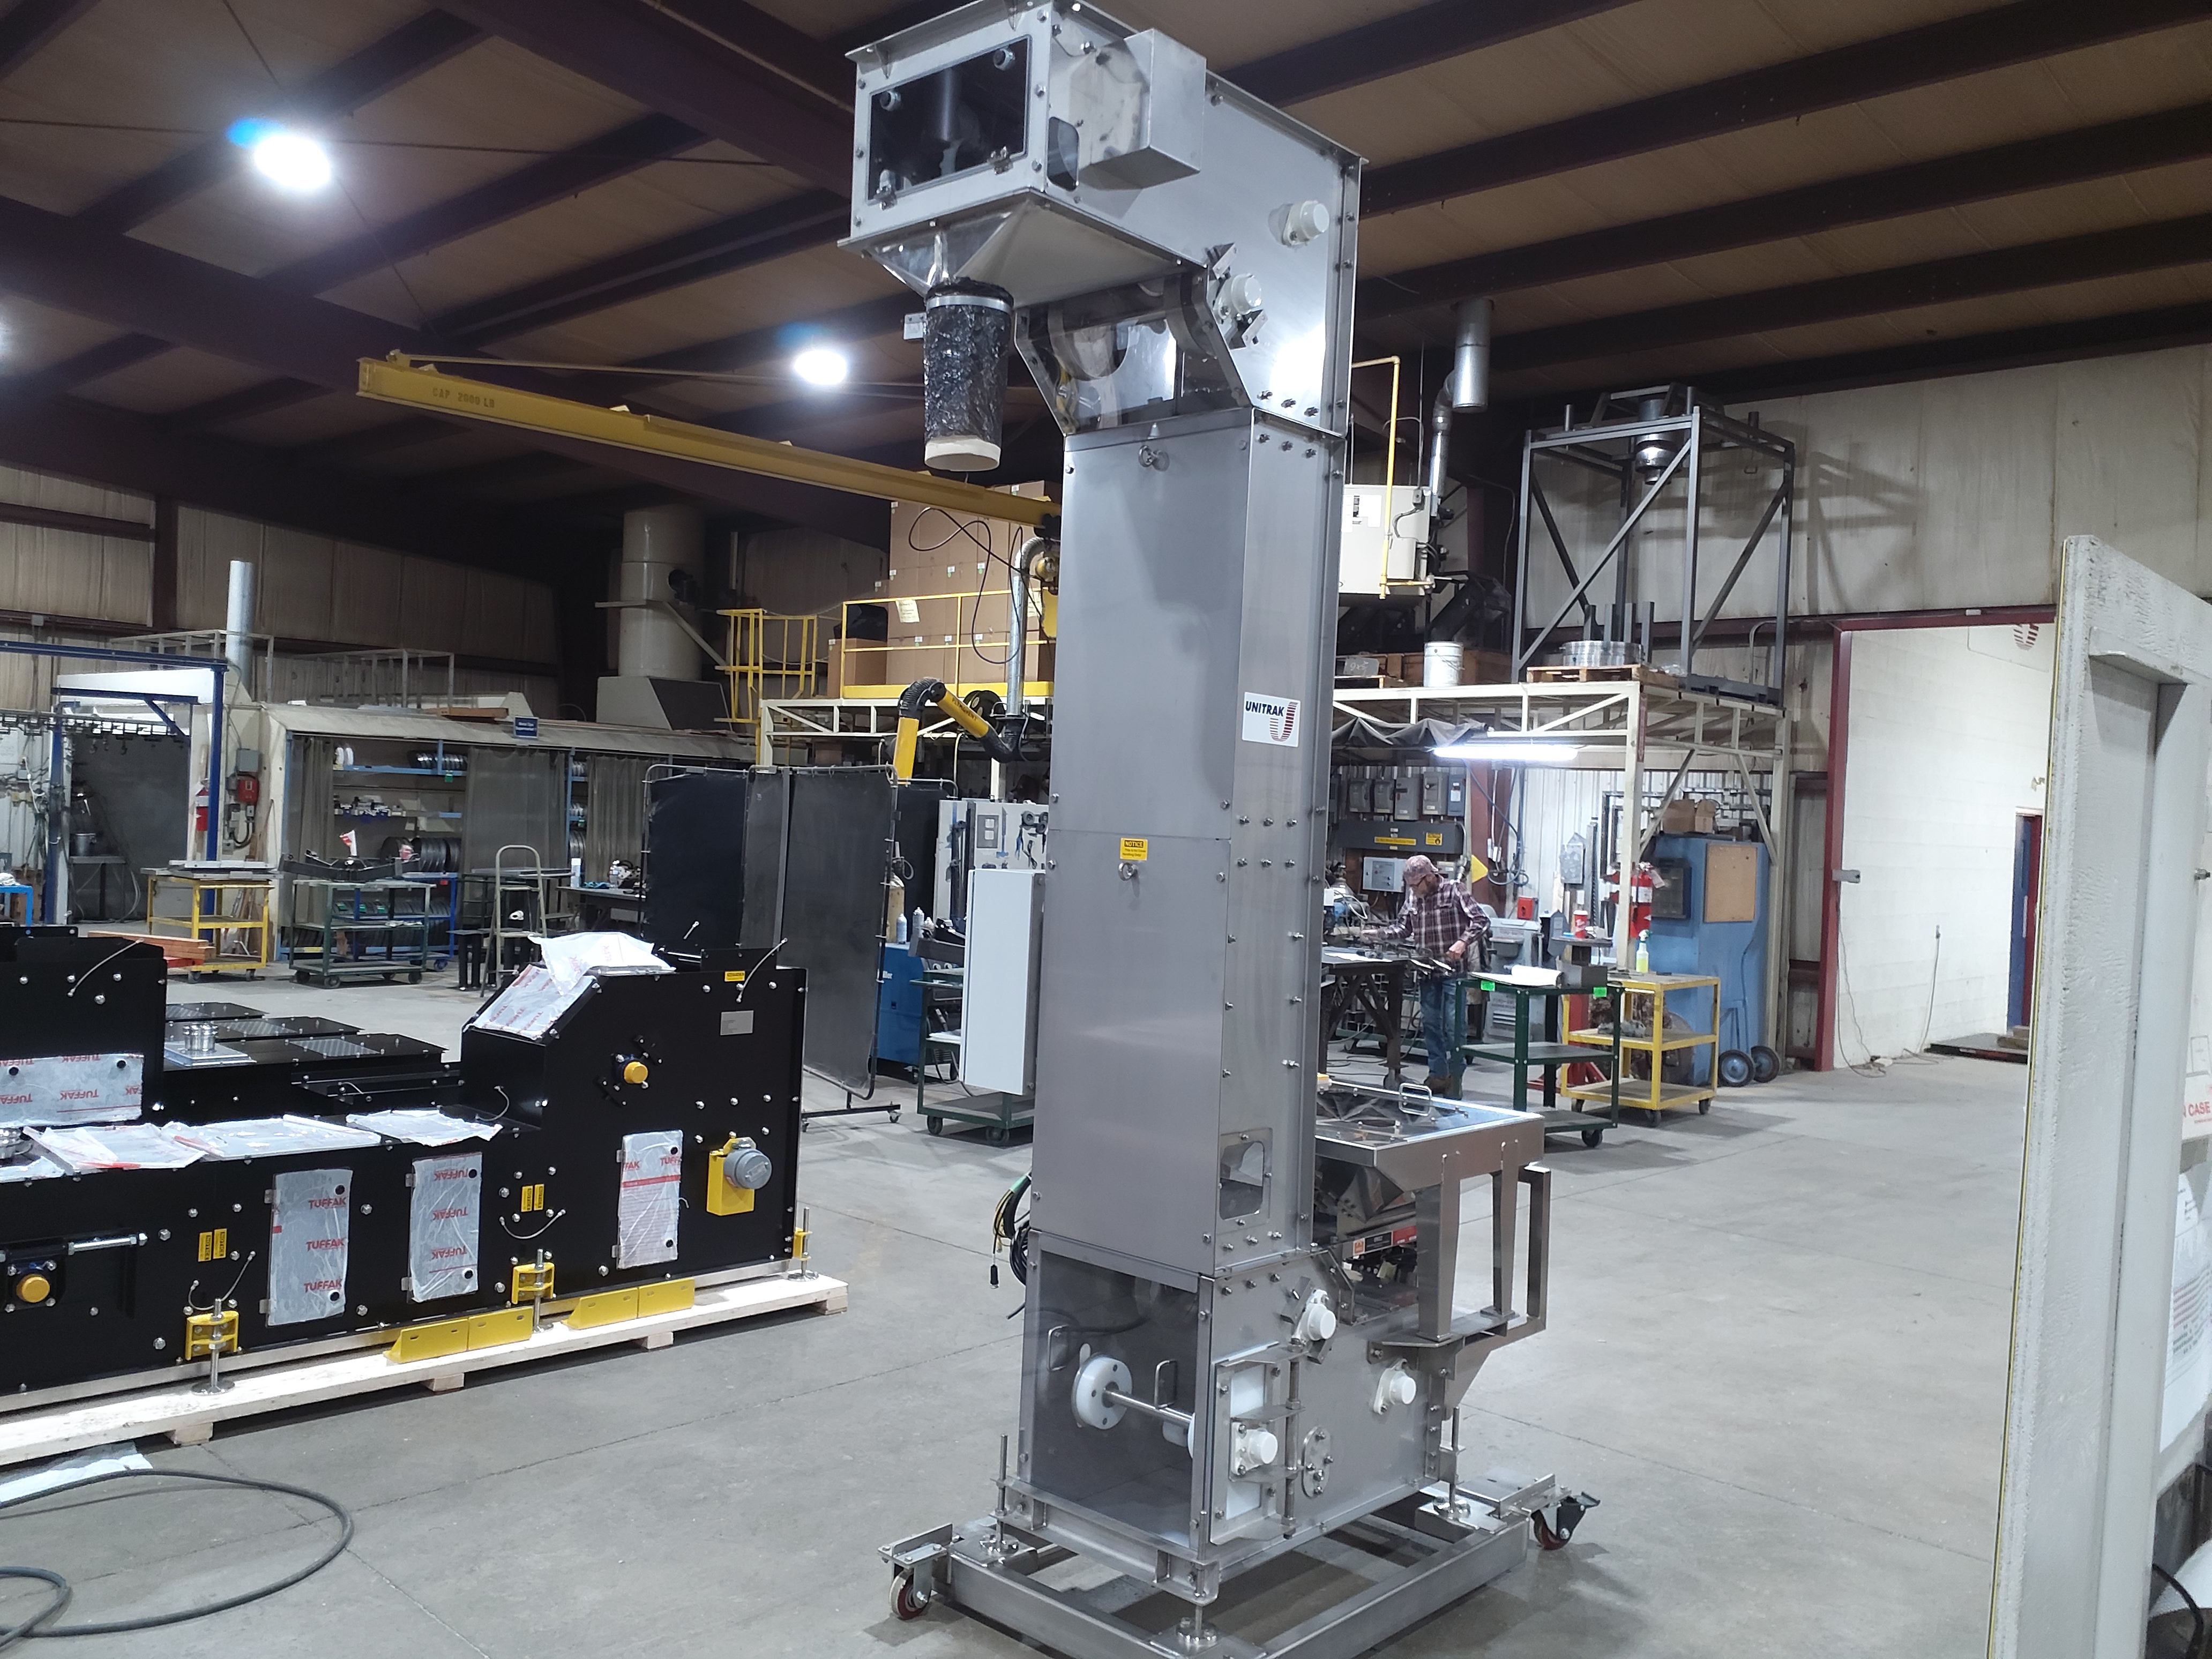
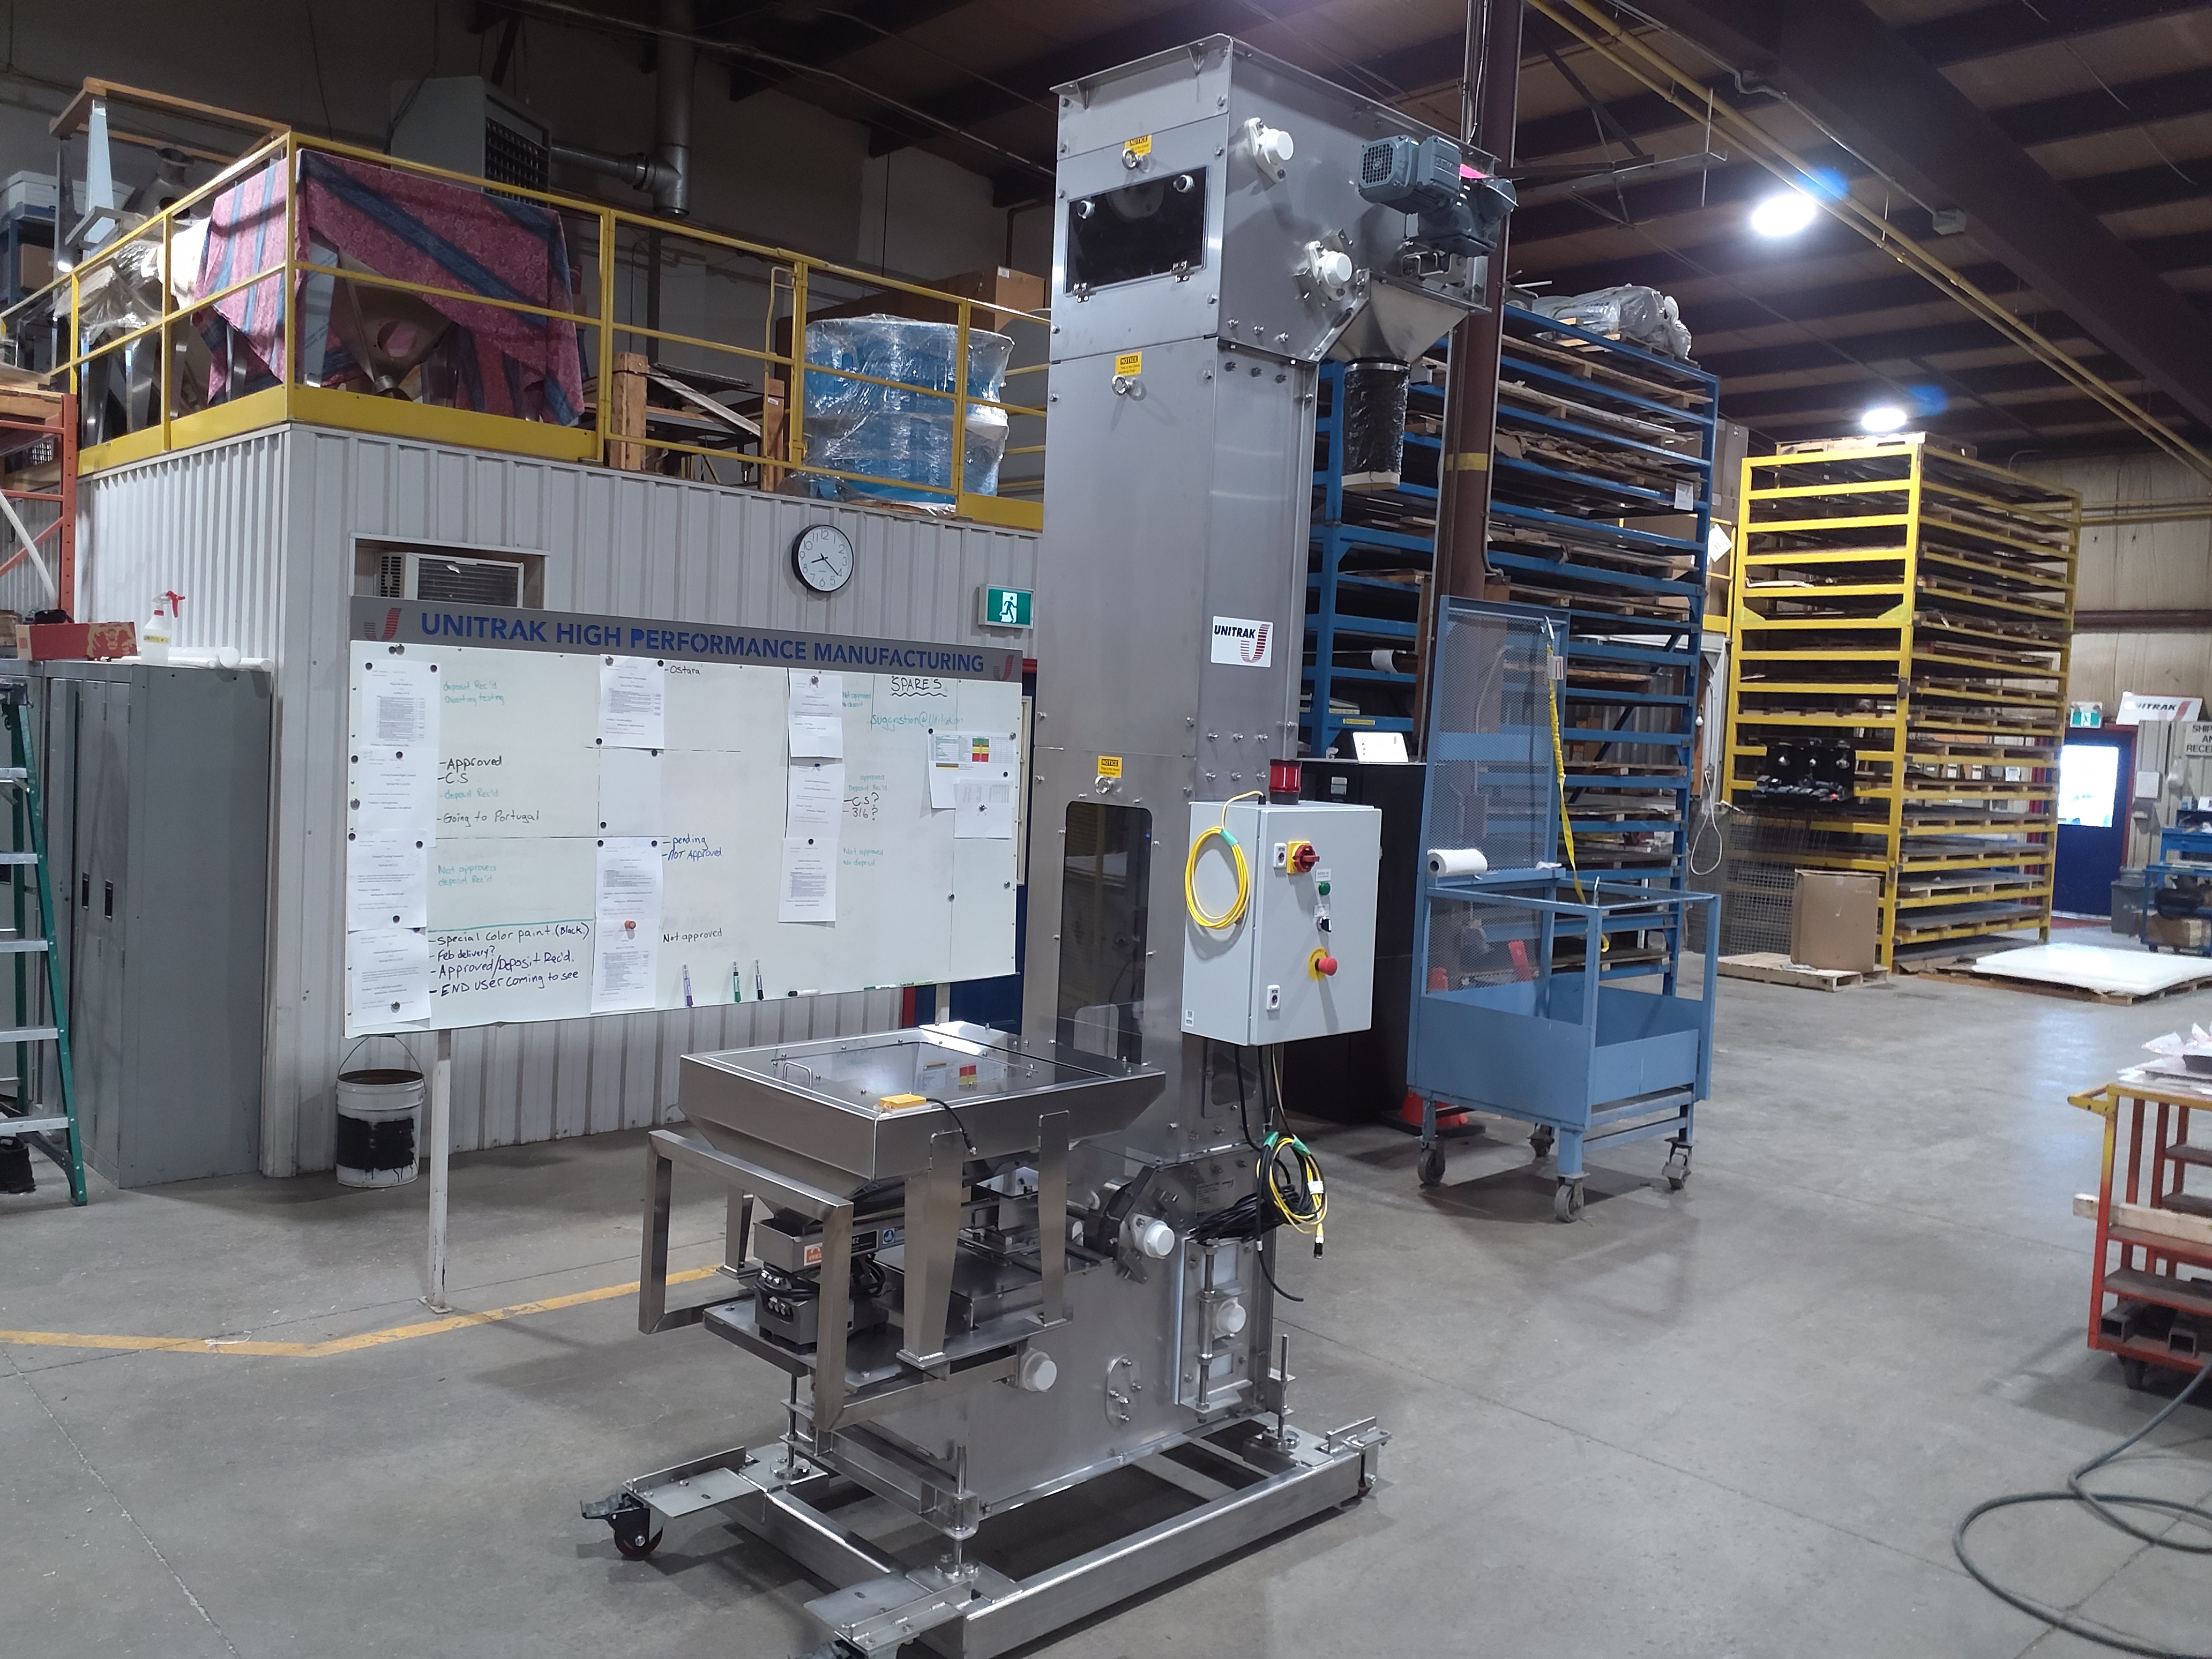
TipTrak™ Bucket Elevator
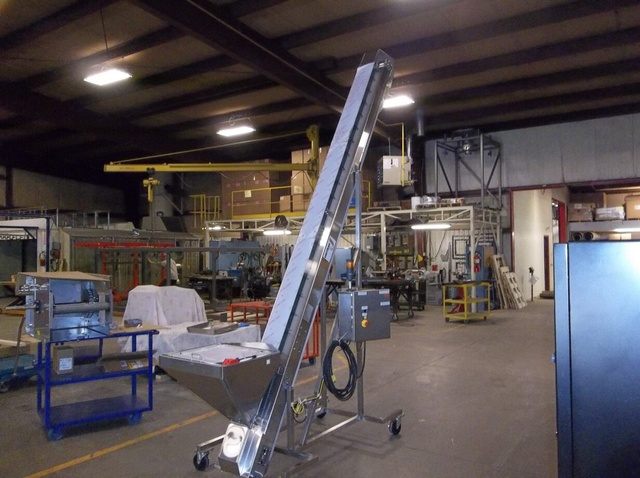
The food grade stainless steel TipTrak™ bucket elevator provided gentle conveying designed to minimize product degradation and prevent breakage of fragile biodegradable valves.
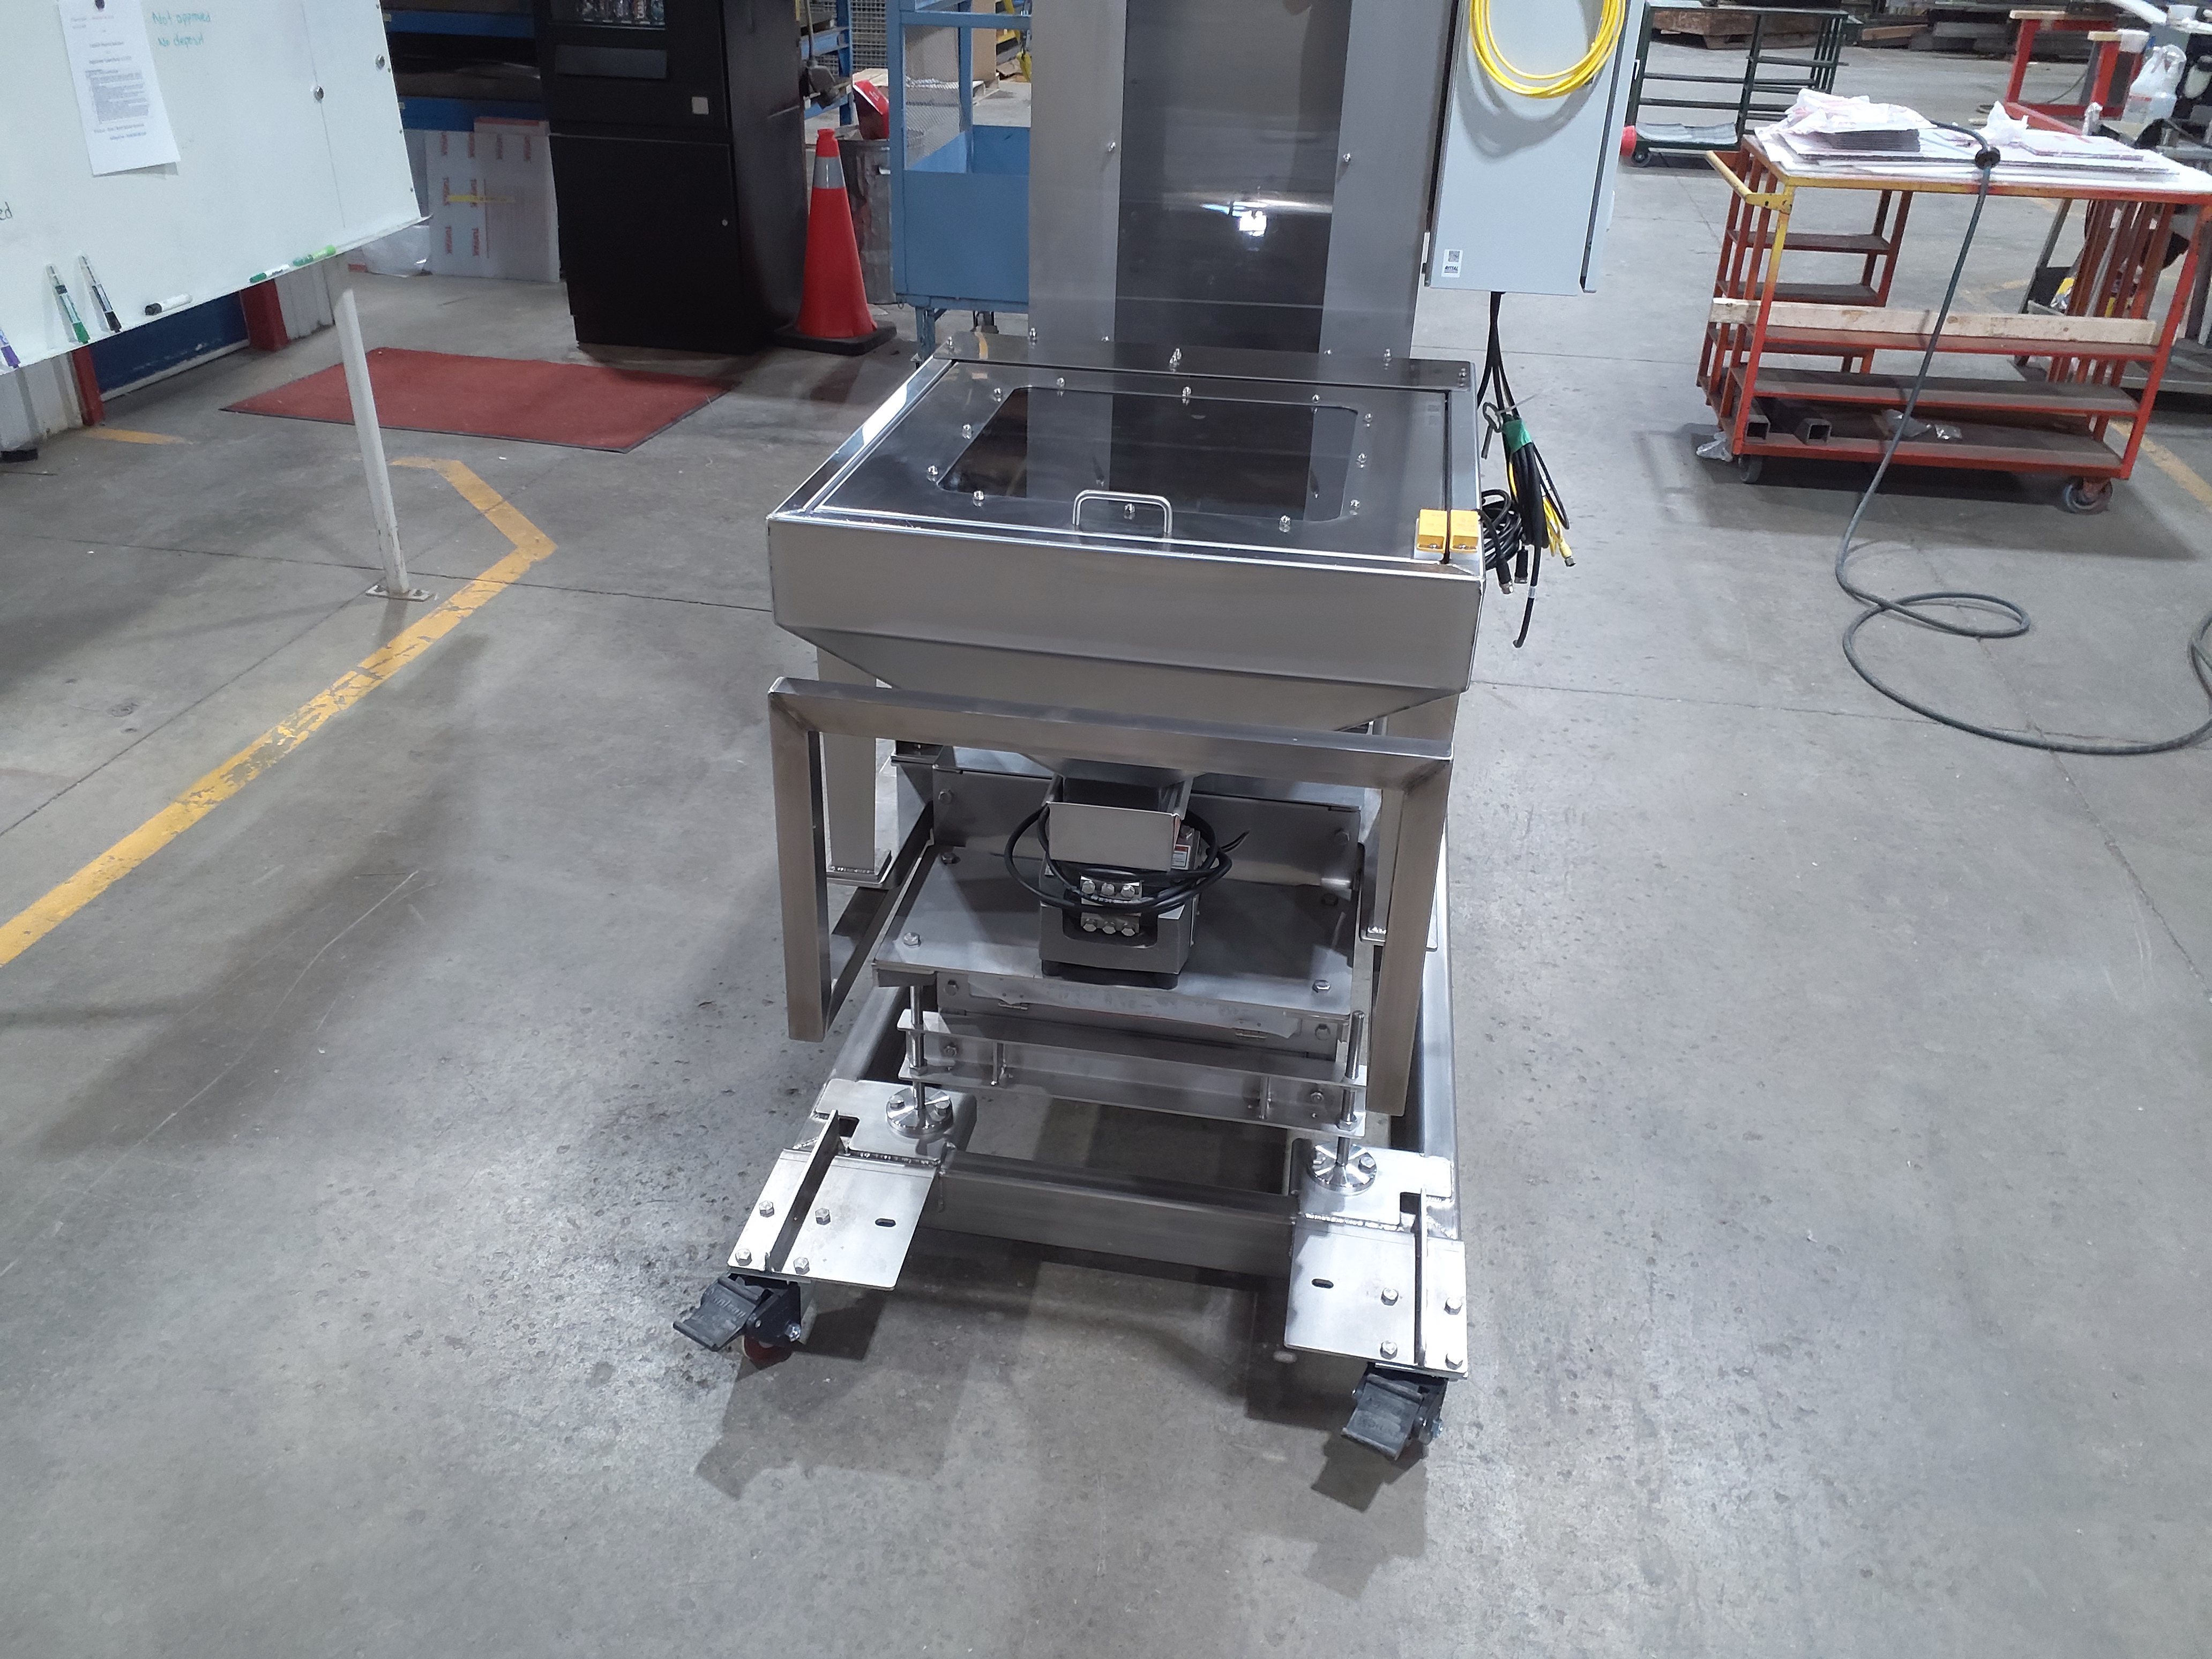
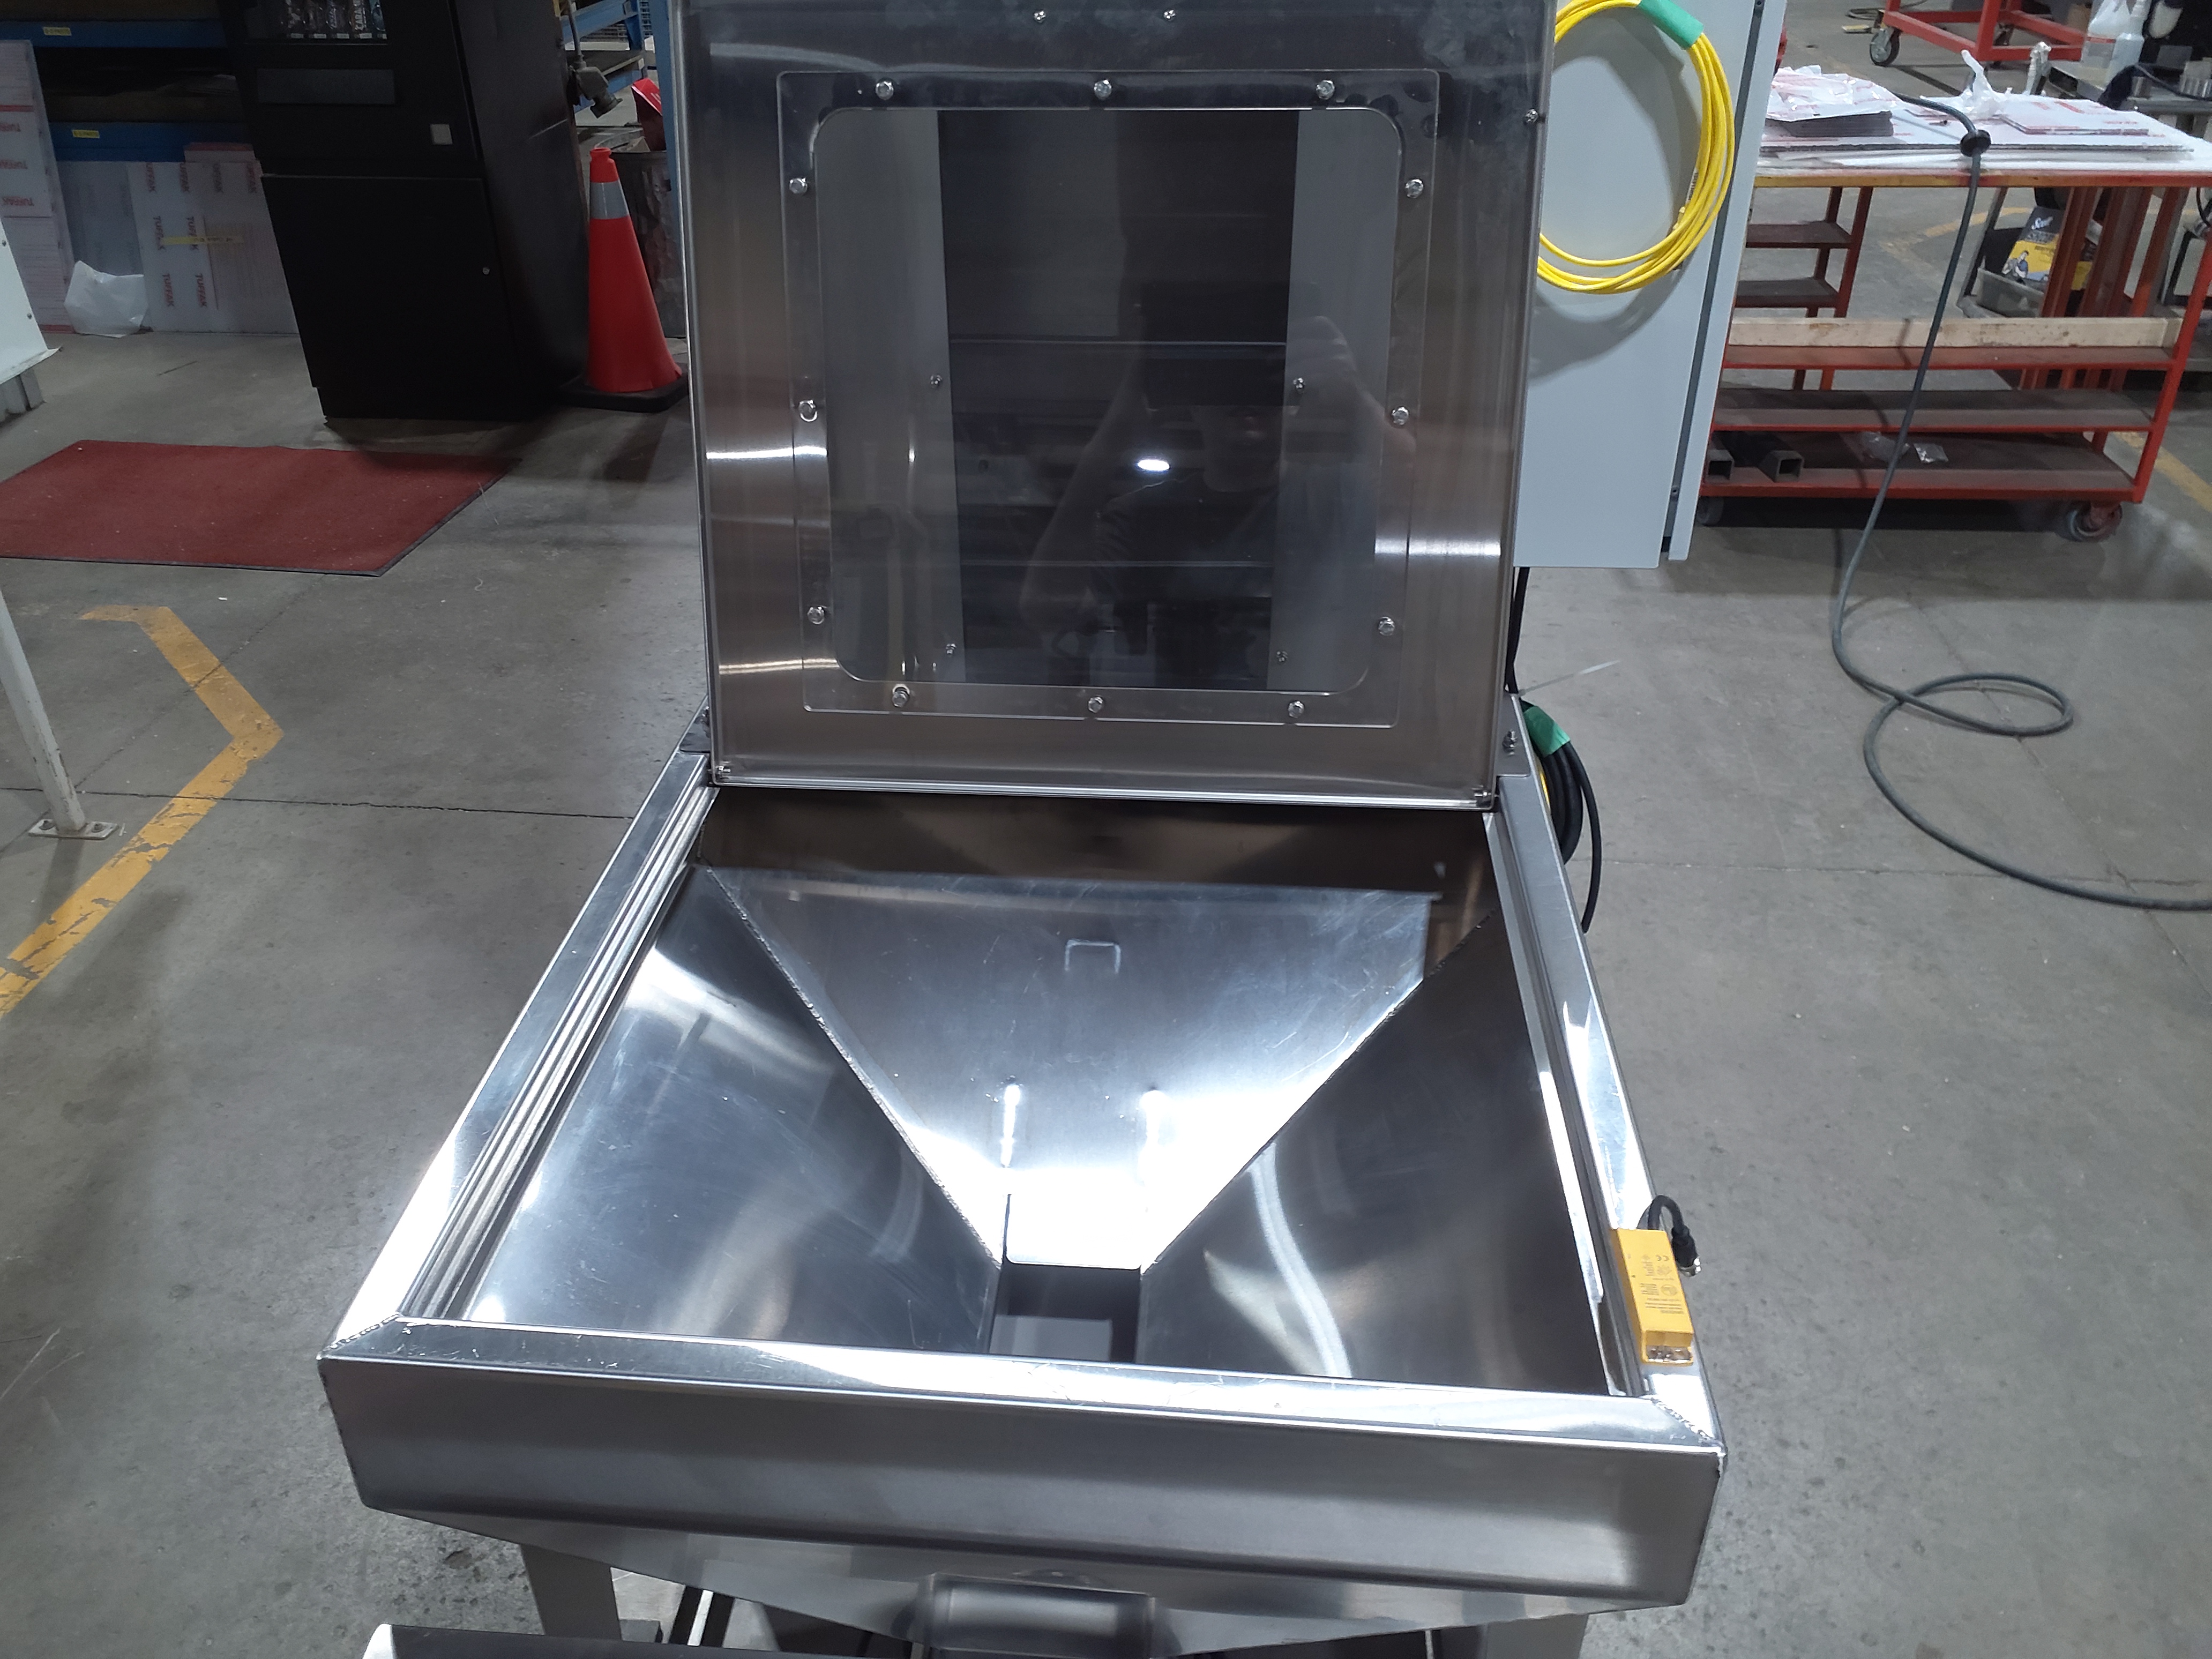
Custom Vibratory Feeder Hopper
A custom feeder hopper delivered controlled product flow from the manual dump area while supporting consistent transfer into the conveying system.
Integrated Controls
Adjustable controls allowed operators to match feed rates with downstream packaging equipment and optimize conveying performance.
Portable System Design
The equipment remained mobile to support aisle access and changing production requirements.