Case Study
Chopped Fibreglass
Johns Manville, a Berkshire Hathaway company, manufactures premium quality building and mechanical insulation, commercial roofing, glass fibersand non-woven materials for…
In this case study
The Challenge
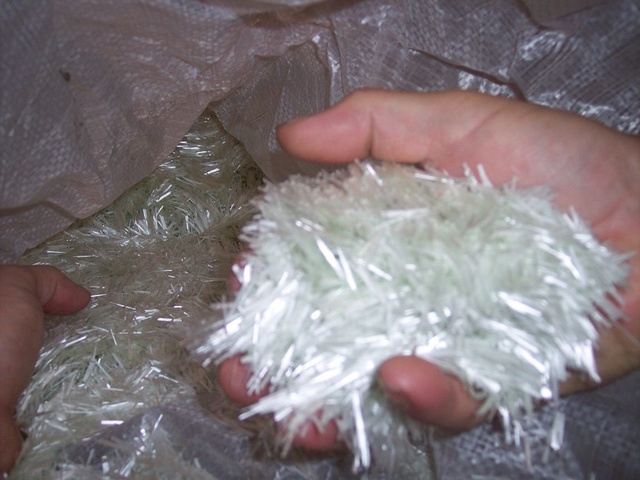
Conveying dried chopped fiberglass is not without its challenges. The product is friable and tends to accumulate static charge when moved or handled. In addition, the light nature of the product makes it susceptible to spillage as it is transported on a conveyor.
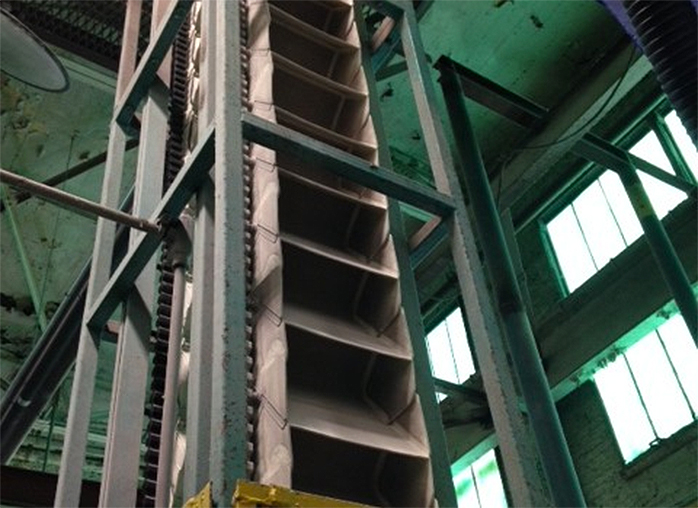
To help Johns Manville select the right conveyor for the job, UniTrak conducted extensive testing of the Johns Manville fiberglass material at its product test facility. This testing showed that TipTrak™ S-5 PEC bucket elevators were an ideal equipment choice for assuring product integrity, preventing spillage and static charge buildup, while achieving the desired throughput rates.
The Solution and Results
Johns Manville is successfully using TipTrak™ conveyors within its production operations at multiple facilities with the USA.
TipTrak™ S-5 units supplied to the Waterville, Ohio and the Cleburne, Texas plants for the handling chopped strand fiberglass have performed with excellent reliability and superior product handling. Equipped with fully conductive options, these conveyors are handling friable product without damage or degradation, and the negative consequences of static charge accumulation have been avoided.
“IT’S VIRTUALLY MAINTENANCE FREE” (ON WHY HE LIKED THE TIPTRAK BUCKET CONVEYOR)”