Technical Article
Total Cost of Ownership: The Most Overlooked Factor in Equipment Purchasing
A true TCO (Total Cost of Ownership) approach looks far beyond sticker price. When evaluating custom conveying equipment, long-term costs like energy use, maintenance, spare parts, labor, and downtime often exceed the initial purchase. This guide explains why TCO is the most important factor in selecting process equipment and how the right vendor can help you reduce operational risk and maximize lifetime value.
In this article
- What TCO Really Includes
- Why TCO Matters in Conveying Equipment
- The Real Impact of Downtime and Operational Costs
- Key Questions Buyers Should Ask Vendors
- Comparison Points That Influence TCO
- 1. Energy Consumption (kWh per ton conveyed)
- 2. Planned Maintenance and Wear Components
- 3. Unplanned Downtime Risk
- 4. Spare Parts Inventory
- 5. Labor for Cleaning and Changeovers
- How TCO Shapes Better Equipment Decisions
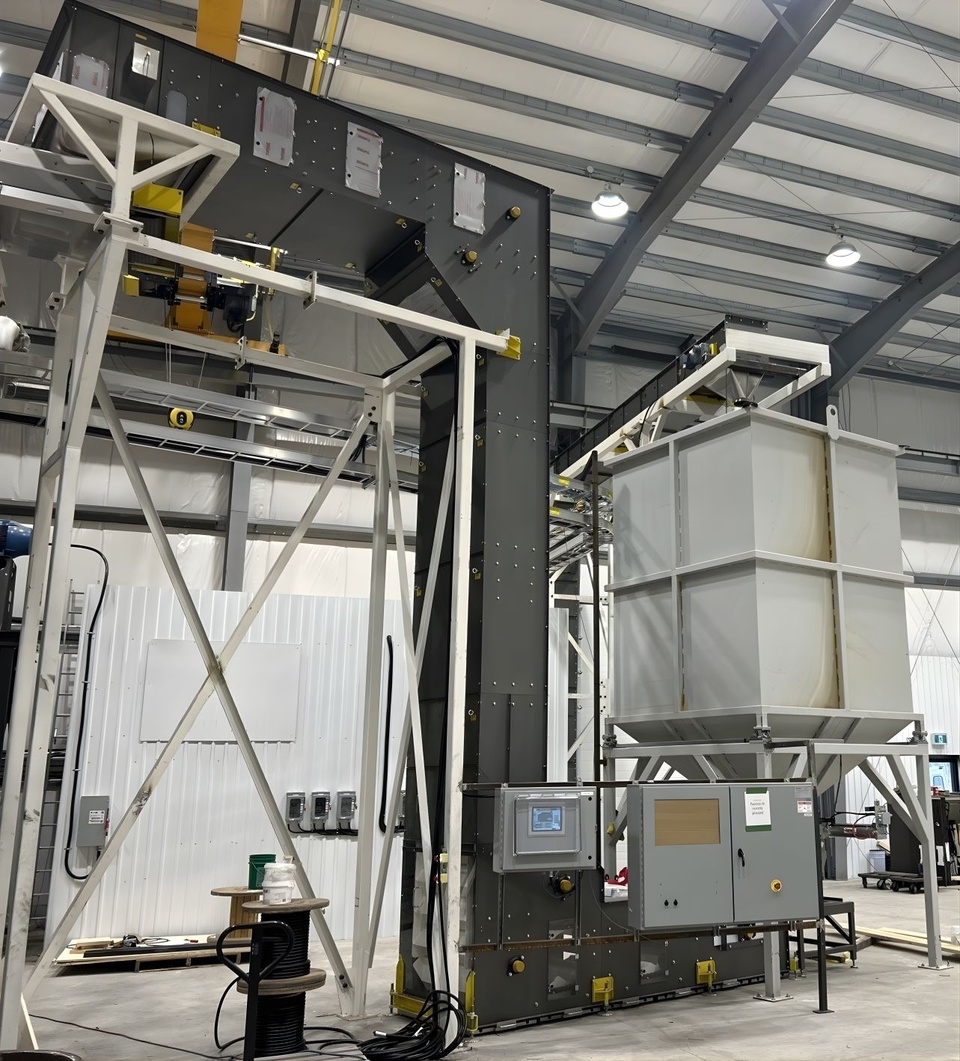
This article is the first installment in a twelve-part series that explores the key considerations manufacturers should evaluate when selecting custom or customized process equipment. Throughout the series, we look at the technical, operational and commercial factors that influence long term performance, reliability, compliance and total value. Each instalment focuses on one essential consideration to help you make confident, well-informed equipment decisions. For further information, or help with your application, please contact our sales team.
When evaluating custom or customized conveying equipment, many buyers still begin with a comparison of sticker prices. Yet almost every serious industrial source now advises against selecting equipment based on upfront capital cost alone. In modern manufacturing environments, long-term performance, reliability, and operational efficiency have a far greater impact on profitability than the initial purchase price.
This is where a Total Cost of Ownership (TCO) framework becomes essential. TCO helps buyers understand the full financial picture across the entire lifecycle of a conveyor or material handling system, not just the cost of day one.
What TCO Really Includes
A true TCO analysis accounts for costs across the full life of the equipment, including:
- Initial purchase
- Installation and commissioning
- Energy use
- Maintenance and service
- Spare parts consumption
- Labor for cleaning, changeovers, and supervision
- Planned downtime
- Unplanned downtime
- End-of-life removal or replacement
Heavy-equipment industries have long adopted TCO frameworks that include fuel or energy consumption, wear and maintenance requirements, depreciation, and resale value. The same approach applies directly to conveying and dry bulk solids handling systems. Decisions made at the equipment selection stage can influence operating costs for decades, especially for manufacturers running multi-shift or continuous production.
Why TCO Matters in Conveying Equipment
Material handling systems often operate for years under demanding conditions. A lower-priced conveyor may seem attractive initially but can generate significantly higher long-term expenses through energy inefficiency, increased maintenance, more frequent downtime, non-standard spare parts, and difficult cleaning processes.
This is especially important in industries handling abrasive, corrosive, friable, or contamination-sensitive materials. Small design differences such as chain style, casing geometry, or flight configuration can meaningfully influence wear rates, sanitation labor, and overall efficiency per ton conveyed.
The Real Impact of Downtime and Operational Costs
Downtime is one of the most expensive hidden costs in industrial environments. Industry studies show:
- Manufacturers experience an average of approximately 800 hours of equipment downtime per year.
- Unplanned downtime costs industrial manufacturers up to 50 billion dollars annually.
- Across the 500 largest global manufacturers, unplanned stoppages can consume 11 percent of annual revenues, totaling roughly 1.4 trillion dollars in lost value.
With costs this high, any equipment decision that reduces downtime or maintenance labor can quickly offset a higher purchase price.
Key Questions Buyers Should Ask Vendors
When comparing options, buyers should evaluate not only what the equipment costs but what it will continue to cost. Helpful questions include:
- Over ten to twenty years, how will total expenses break down between capital, energy, maintenance, labor, and downtime?
- How does the vendor model TCO? Do they present realistic operating scenarios and lifecycle cost projections rather than a single line-item quote?
- What consumables or wear parts are expected and at what intervals?
- How long does planned maintenance typically take and can components be serviced without specialized tools or extensive teardown?
- What does the vendors service network look like? Response time, parts availability, and technical support directly affect unplanned downtime risk.
A vendor that cannot clearly articulate lifecycle costs may put your operation at unnecessary risk.
Comparison Points That Influence TCO
When evaluating different conveying technologies or custom design options, consider these cost drivers:
1. Energy Consumption (kWh per ton conveyed)
Mechanical conveyors are generally more energy efficient than pneumatic systems because they move material directly rather than moving air. Dense-phase pneumatic conveying can be competitive in certain niche applications but typically adds complexity and higher capital cost.
2. Planned Maintenance and Wear Components
Assess the expected life and cost of:
- Chains, belts, or cables
- Sprockets and bearings
- Flights, wear plates, liners
- Lubrication systems
- Recommended overhaul intervals
Standardized and easily accessible components reduce service time and long-term spending.
3. Unplanned Downtime Risk
Simpler, robust mechanical systems with fewer critical wear points generally experience fewer breakdowns than highly complex or proprietary designs.
4. Spare Parts Inventory
Consider:
- Number of unique part numbers
- Whether components are standardized across multiple lines or models
- Vendor lead times
- Availability of rapid shipment
Spare parts represent the largest share of maintenance cost over time, so standardization yields major savings.
5. Labor for Cleaning and Changeovers
Sanitary or easy-access designs can significantly reduce labor hours, improve hygiene, and shorten production resets. In regulated industries such as food, nutraceuticals, or specialty chemicals, this can be a decisive advantage.
How TCO Shapes Better Equipment Decisions
A TCO-driven purchasing process leads to better long-term outcomes by prioritizing:
- Reliability
- Predictability
- Efficiency
- Maintainability
- Lifecycle support
For manufacturers handling bulk solids and powders, conveying equipment is not simply a capital purchase. It is an operational asset that influences throughput, quality, and profitability for decades.
Selecting partners who understand and communicate full lifecycle cost is one of the most effective ways to reduce operational risk and maximize return on investment.
At UniTrak, we design conveying solutions with lifecycle performance at the forefront, not as an afterthought. Our equipment is built to deliver predictable, long-term value through reliable operation, reduced maintenance burden, and proven durability across thousands of materials and applications. If you are evaluating options or want help modelling the true cost of ownership for your project, our sales engineering team is here to support your decision-making with data, application expertise and transparent guidance. Talk to us about your application and let us help you select the right long-term solution.
In our next article in this series we explore: Application & Material Fit.