Technical Article
Conveying Sulfur Prills, Pastilles and Pellets
Conveying sulfur requires more than moving material at the required rate. Broken prills and pastilles create fines, spilled product adds cleanup, and dust introduces hazards that must be addressed throughout the installation.
In this article
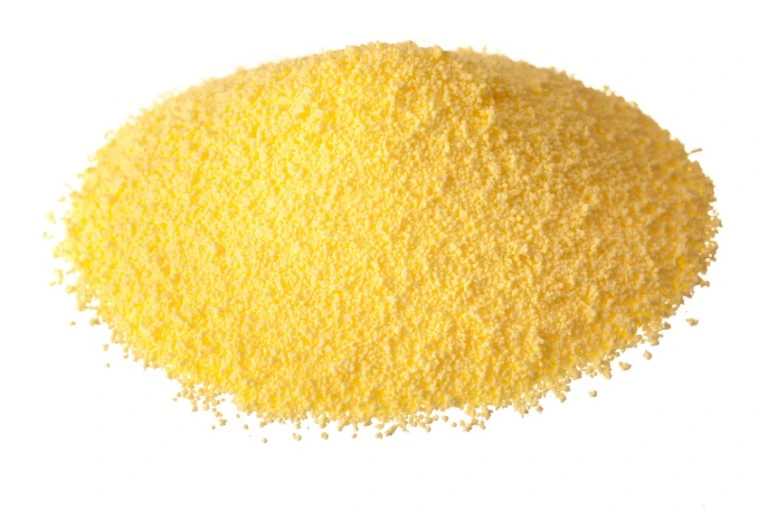
The right conveyor should protect the formed product, control product loss and provide construction suited to the material and operating environment.
Sulfur, also spelled sulphur, is handled in several solid forms. Understanding their differences helps establish the feeding, conveying and discharge arrangements.
What are sulfur prills, pastilles and pellets?
Prills are small, generally rounded particles formed by cooling droplets of molten material until they solidify. Sulfur prills can be produced using air or wet prilling processes.
Sulfur pastilles are formed by depositing molten droplets onto a cooled belt. The droplets solidify into rounded pieces with a flattened base.
Sulfur granules can be produced by building up layers of sulfur around seed particles. Pellet is a broader commercial term, so the product name alone may not establish its shape, strength or handling characteristics.
These differences matter when selecting a conveyor. Obtain the actual particle-size distribution, bulk density, temperature, moisture content and proportion of fines rather than designing around a generic description of “solid sulfur.”
Material behavior: protect the product and maintain flow
Forming sulfur into prills, pastilles or granules makes it practical to handle as a bulk solid. However, the material can still break down during loading, conveying and discharge.
Repeated drops and unsuitable handling conditions can increase fines. That affects product quality and adds to the dust-management burden.
Review the complete route, including:
- The drop from upstream equipment into the conveyor.
- Normal and peak feed rates.
- Horizontal conveying distances and vertical lift.
- Changes in direction and intermediate transfers.
- Discharge into bins, packaging equipment or the next process.
Flow behavior also needs checking. Moisture, fines and storage conditions can affect feeding and discharge. Do not assume that every sulfur grade will remain free-flowing under the conditions in your plant.
Materials of construction require similar attention. Assess wear exposure and chemical compatibility using the actual sulfur grade, contaminants, moisture and operating temperature. Stainless steel and other component options should be selected around those conditions.
Sulfur dust and ignition considerations
Sulfur is combustible, and finely dispersed sulfur dust can form an explosive mixture in air. Handling solid prills or pastilles does not remove the need to assess dust generated during conveying.
Equipment selection must reflect the site’s hazard assessment and the applicable requirements for the installation.
That assessment should address dust containment, potential ignition sources, electrostatic charge, equipment monitoring and any required explosion protection or isolation. It must also cover the connections between the conveyor and surrounding equipment.
A dust-tight enclosure provides containment. It does not, by itself, establish explosion protection. Likewise, fitting an explosion-proof motor does not establish the suitability of the complete conveyor.
Where ATEX requirements or hazardous-location electrical classifications apply, confirm the specific equipment configuration and documentation required for the application.
Reducing breakage and unnecessary transfers can help limit additional dust generation. These measures support the wider dust-management strategy.
Which conveyor types suit sulfur handling?
Select the technology around the sulfur form, throughput, route, acceptable degradation and assessed hazards. Compare how each proposed conveyor loads, carries and discharges the material.
TipTrak bucket conveyors: protect formed sulfur through the conveying route
TipTrak bucket conveyors are a strong fit where preserving sulfur prills, pastilles and pellets matters alongside elevation and containment.
Low operating speed helps protect particle integrity. Compared with the relatively high-speed discharge of a centrifugal bucket elevator, TipTrak offers a different handling approach for formed products sensitive to breakage.
Interlocking buckets control product loss. The buckets remain connected throughout the conveying path, including the vertical lift, supporting spill-free conveying within the specified application conditions.
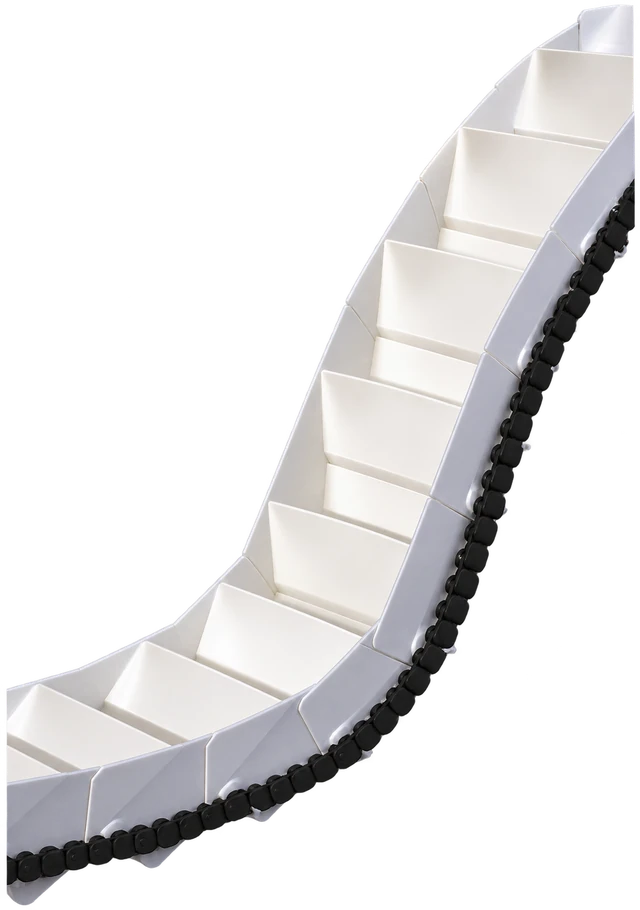
Horizontal and vertical conveying from one drive eliminates intermediate conveyor transfers. A route assembled from separate conveyors introduces additional discharge and reloading points. TipTrak connects those sections within one conveying system, reducing repeated drops and the number of transfer interfaces requiring containment.
The reinforced rubber beltchain reduces routine chain maintenance. It uses pre-tensioned aircraft cables and has no conventional roller-chain joints requiring lubrication. The reinforcement also resists stretch and reduces tensioning requirements.
For sulfur handling, these advantages work together: gentle movement helps limit additional fines, interlocking buckets retain product, and fewer transfers simplify the conveying route.
TipTrak requires controlled feed. Match the inlet and feeding equipment to the material, capacity and upstream process.
Monocoque construction for containment requirements
TipTrak Monocoque provides dust-tight construction for applications requiring containment. Conductive construction options and purge-capable designs are available where applicable.
Select the enclosure, bucket assembly, beltchain materials and seals around the sulfur grade and operating conditions. Specify the conveyor’s construction and components to match the application, and coordinate its interfaces with the site’s dust-management and explosion-protection systems.
The required configuration follows the assessed application. Monocoque construction alone does not establish a particular ATEX classification or explosion-protection capability.
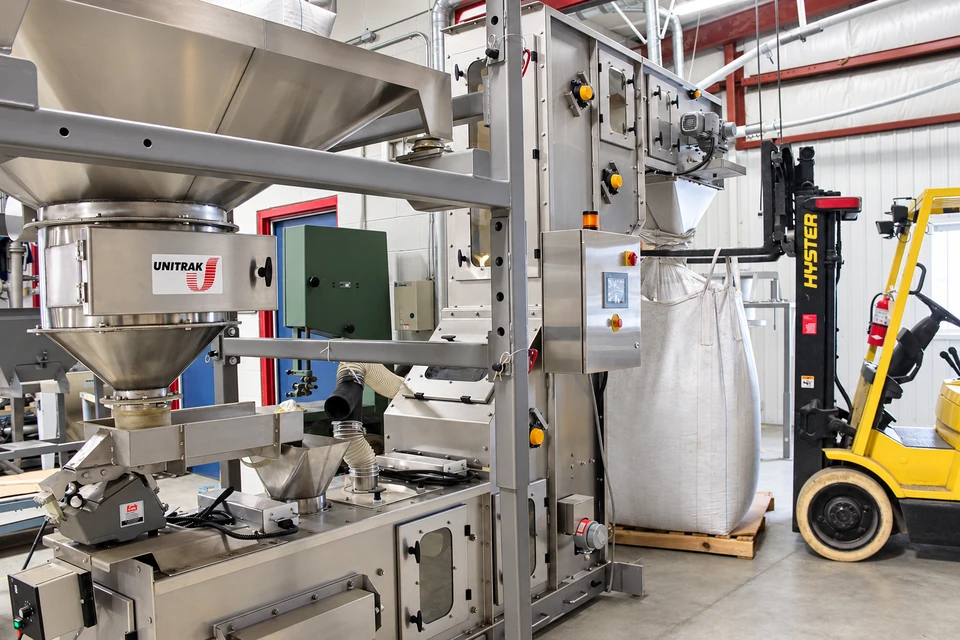
Powderflight aeromechanical conveyors: compact, enclosed transfer
Powderflight provides enclosed conveying through tubes, with high throughput relative to equipment size and horizontal, vertical or angled configurations.
It offers an alternative where space and transfer rate are central to the requirement. Its high-speed rope-and-disc operating principle differs from TipTrak’s low-speed bucket movement.
For sulfur prills and pastilles, assess acceptable breakage and fines generation before selecting an aeromechanical conveyor. Sulfur suitability also requires review of component compatibility and the application’s assessed hazards.
Where preserving fragile formed particles is the main priority, TipTrak’s low operating speed and connected bucket path provide a clear basis for evaluation. Where compact transfer is the main constraint, Powderflight may warrant assessment.
Belt, screw and pneumatic conveyors
Other technologies may suit particular parts of a sulfur-handling process.
Belt conveyors may accommodate horizontal transport. Screw conveyors move material through contact with a rotating screw, while pneumatic systems use an air stream. Their loading, contact and discharge conditions differ.
Compare the proposed installation for particle degradation, containment, wear, maintenance and transfer requirements. A conveyor that meets the capacity target can still create unacceptable fines or cleanup demands.
UniTrak’s sulfur-handling experience
UniTrak has supplied TipTrak bucket conveyors for sulfur pastilles, granules and prills.
That experience informs the review of component compatibility, containment, feed control and conveying layouts. Relevant previous applications can support equipment selection, while the proposed system must address the material and conditions at your facility.
For more on conveyor types, configurations and sizing, read our bucket elevator design and selection guide.
Discuss Your Application
Selecting a sulfur conveyor starts with the material and the process.
Provide:
- Sulfur form, particle size and proportion of fines.
- Required throughput and bulk density.
- Operating temperature and moisture content.
- Horizontal distances, vertical lift and discharge locations.
- Current safety data sheet.
- Available dust-hazard assessment and hazardous-area classification information.
Discuss Your Application with UniTrak to review TipTrak, Powderflight and the appropriate conveying configuration.